Find equipment by installation point and separation task.
All magnetic separators →Start with the material or production line you need to protect.
All applications →Compare technologies, check parameters and prepare your RFQ.
All guides →See the factory, quality checks and answers before you request a quotation.
The Corvelan LJT-H is an underbelt conveyor metal detector for finding unwanted ferrous and non-ferrous metal on moving conveyor lines. The sensor sits below the belt, giving you a compact conveyor belt metal detector where a full detector tunnel may not fit.
Confirmed LJT-H-2 models on this page cover 500–1600 mm belt widths and 0.5–4.5 m/s belt speeds. Flat-type and V-type sensors are available for different conveyor profiles.

Start with the conveyor layout and the metal you need to find. The LJT-H is a practical starting point when the sensor can sit below the belt and the main job is metal detection rather than automatic removal.
The LJT-H sensor installs under the conveyor belt. It does not need a full tunnel around the conveyor.
The compact underbelt layout can fit where there is not enough room for a larger detector around the belt.
The LJT-H is a better starting point when larger loose metal pieces are the main concern. We do not assume fine-particle detection without a defined test.
The LJT-H detects metal but does not remove it by itself. Tell us what should happen after detection so we can review the required control setup.
On bulk conveyor lines, unwanted metal can move with the material toward downstream machines. In this role, the LJT-H works as a tramp metal detector: it identifies the metal early enough for the line controls to respond before the metal travels farther through the process.
The detector identifies unwanted metal while it is still on the conveyor, before the material reaches the next process step.
Depending on the selected controls, a detection signal can be used for an alarm, conveyor stop, marker or a separate reject action.
Earlier detection can help reduce the risk of unwanted metal continuing into crushers, shredders or other downstream equipment. The actual protection result still depends on the full line design and response method.
The confirmed LJT-H application references available to us are plastics, wood and quarry conveyors. We still check the material, belt profile, material depth and target metal before we recommend a setup.
Use the LJT-H where plastic material moves on a conveyor and unwanted metal needs to be found before the material continues to the next process. Send the belt width, material depth and target metal so we can review the setup.
We review the wood material, normal material depth, belt shape and target metal before recommending the detector. If the required target is small or may sit far from the sensor, define it before selection.
Use the underbelt detector where loose metal needs to be found on a quarry conveyor and the compact sensor can fit below the belt. Conveyor structure and available space should be checked before installation.
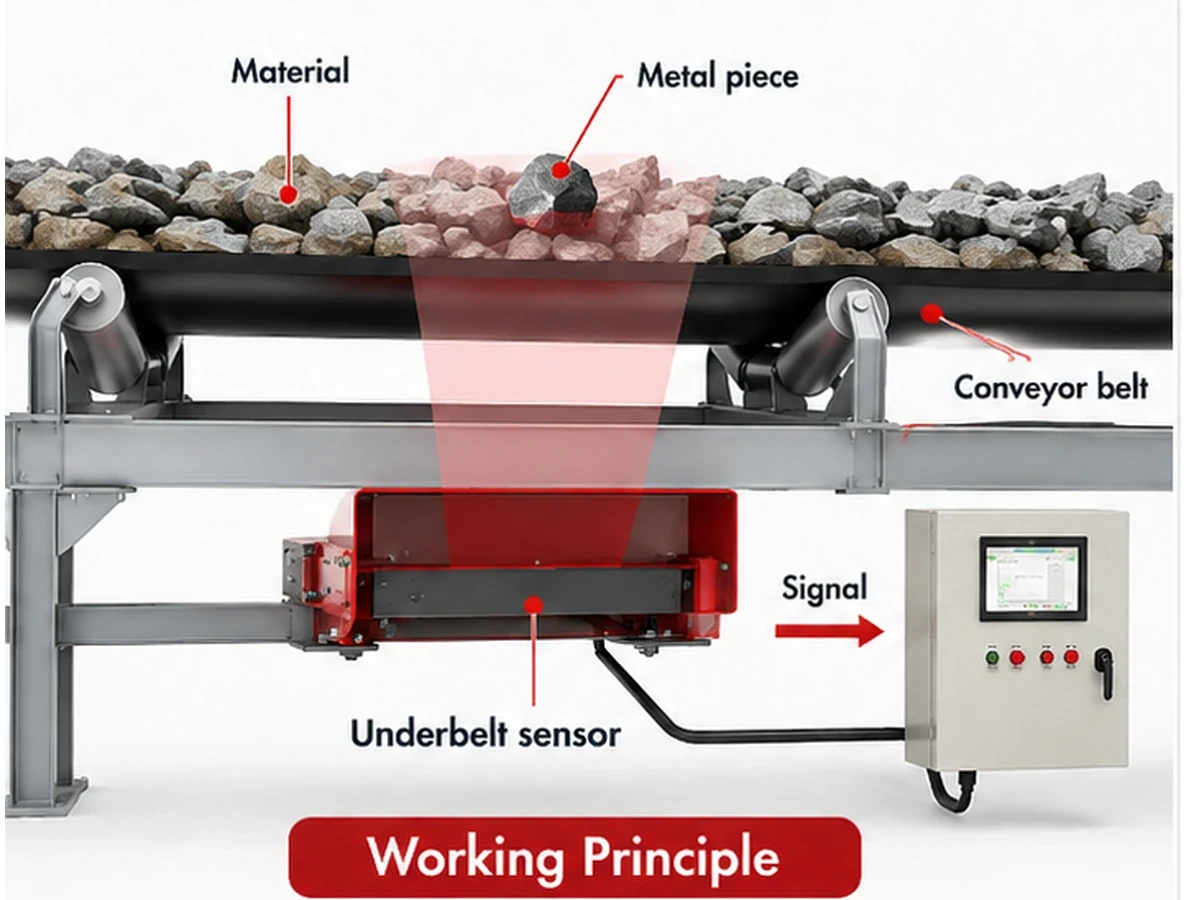
The sensor sits below the belt and creates an electromagnetic detection zone through the belt and the material above it. When metal enters that zone, the detector produces a signal that can be used by the control system.
The conveyor carries material above the underbelt sensor at the normal operating speed and material depth.
When ferrous or non-ferrous metal passes through the sensing area, the detector signal changes.
Depending on the selected controls, the signal can be used for an alarm, conveyor stop, marker or a separate reject system.

There is no single sensitivity number that describes every conveyor. Detection depends on the target metal and the real conditions between the metal and the underbelt sensor.
Metal type, mass, shape and orientation change the detection signal.
What to send: metal type plus an example size, photo or test piece if available.
A metal piece close to the sensor is usually easier to detect than the same piece farther away.
What to send: the most difficult expected metal position in the material layer.
A deeper layer puts some metal farther from the sensor. Engineers often call this material depth the burden depth.
What to send: normal and maximum material depth.
The confirmed LJT-H-2 range on this page is 0.5–4.5 m/s.
What to send: normal operating speed and any major variation.
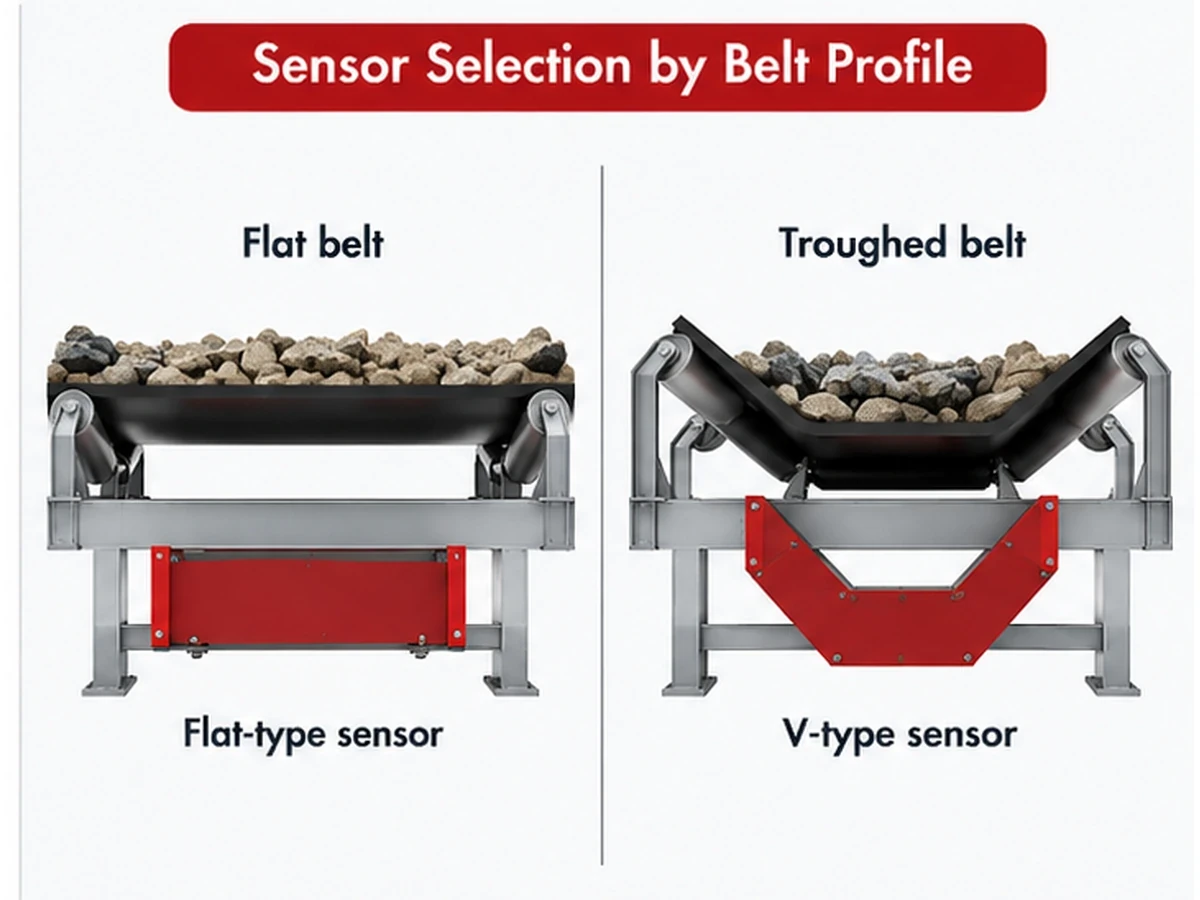
Flat-type and V-type sensors are available. We choose the sensor shape to match the conveyor profile.
What to send: belt profile, trough shape and a photo or drawing.
Nearby steelwork, idlers, cables, vibration and electrical noise can affect where the detector should be installed.
What to send: photos and dimensions around the planned detection point.
We start with the conveyor and the metal you need to find. Belt width is important, but it is not enough by itself.
| What to Check | Why It Matters | What to Send Us |
|---|---|---|
| Material & material depth | Material depth changes how far the metal can be from the sensor. | Material name, normal/max depth, particle or piece size if known. |
| Target metal | Metal type, size, shape and position can change the signal. | Example metal, photo, sample description or required test piece. |
| Belt width & profile | They guide sensor size and whether a flat-type or V-type sensor fits better. | Belt width, profile, conveyor photo or drawing. |
| Belt speed | It changes the time the target spends in the sensing zone. | Normal and maximum operating speed. |
| Available installation space | The detector must fit around the frame, idlers, covers and maintenance access. | Side/front photos, dimensions and available clearance. |
| Belt joint / splice | A belt joint that contains metal can affect detection or control settings. | Splice type and whether it contains metal. |
| What should happen after detection? | The signal must connect to the action you need. | Alarm, conveyor stop, marker, separate reject system or control-system connection. |
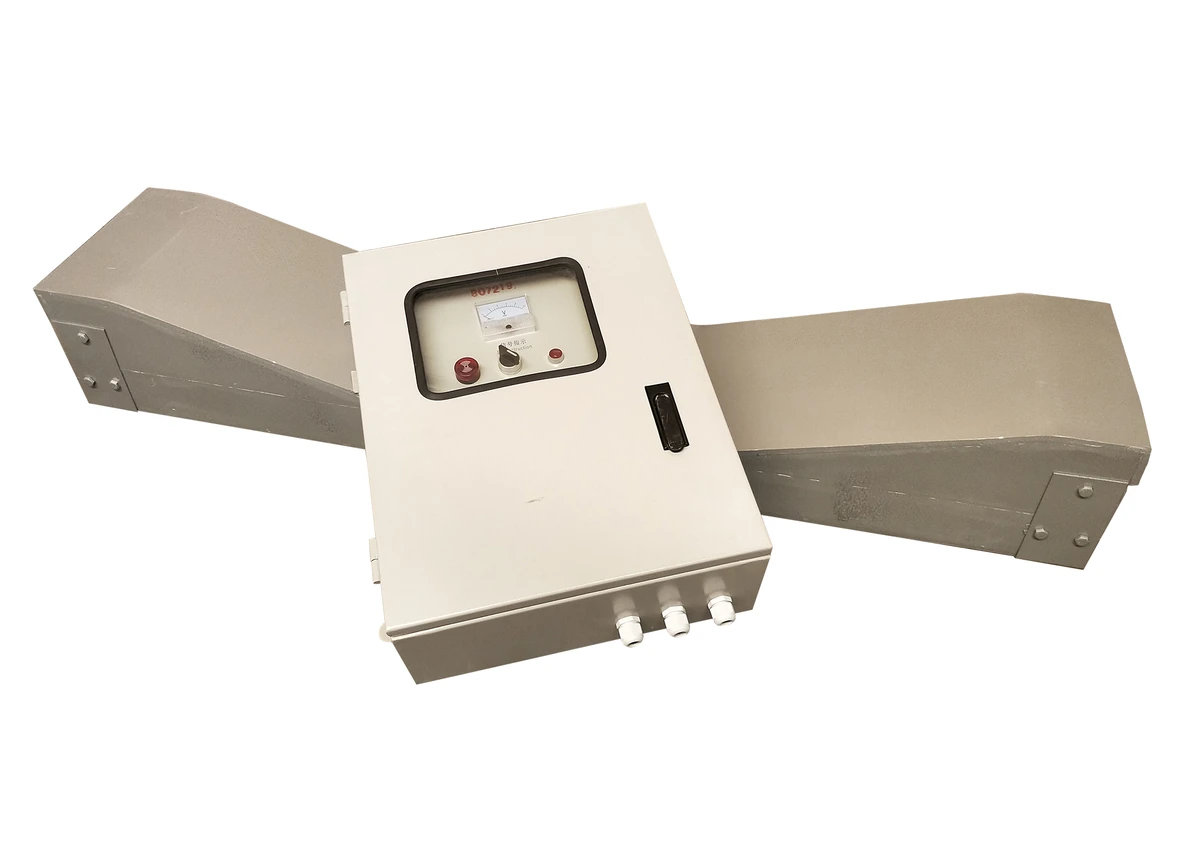
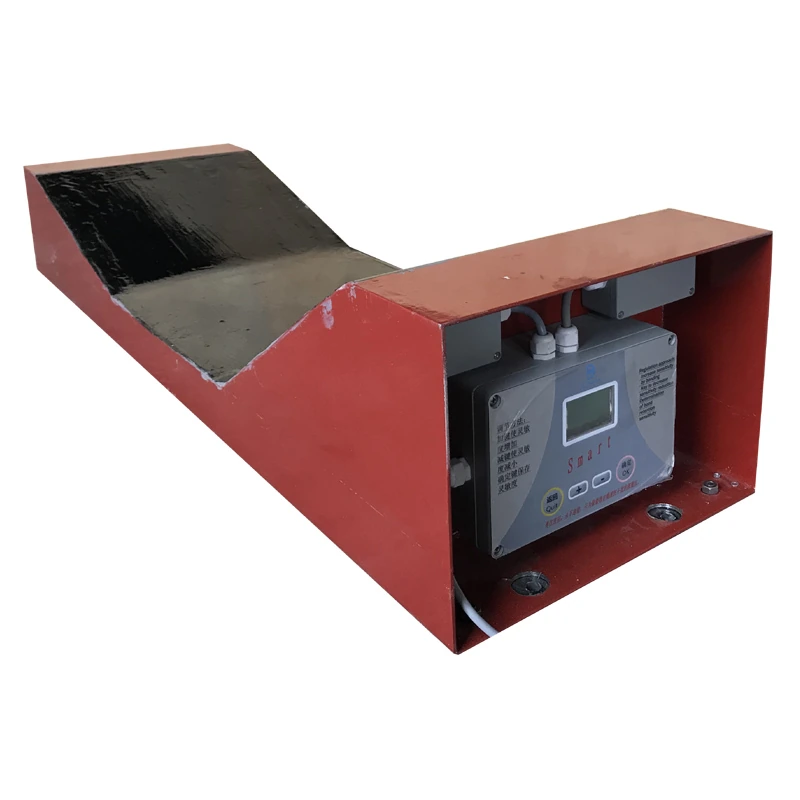
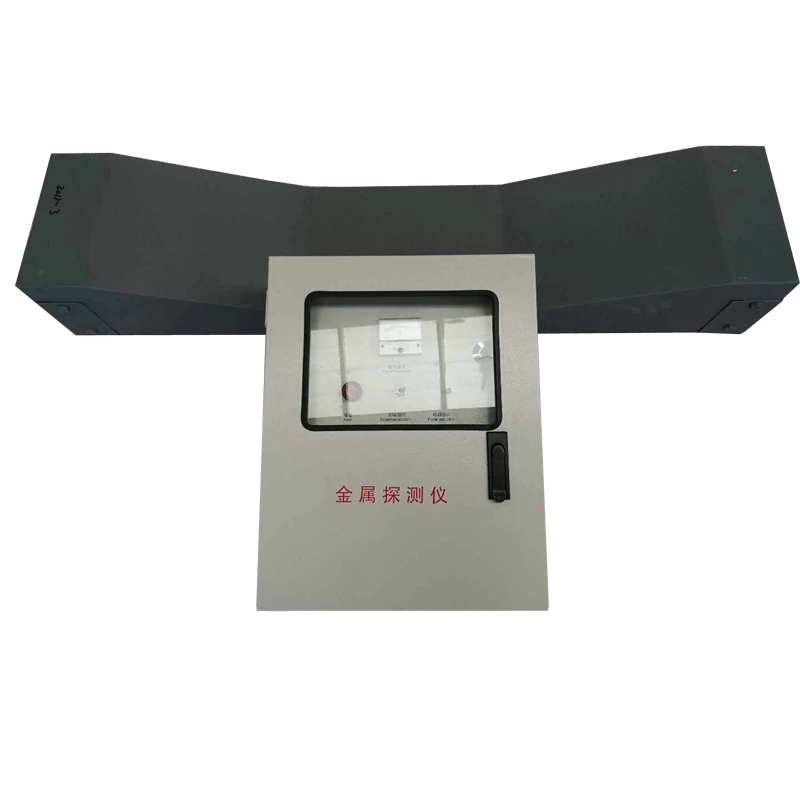
The LJT-H family includes flat-type and V-type sensors. We choose the sensor form from the conveyor profile. Electronic control-unit choices and an optional belt-joint detector are also listed for the product family. We confirm the exact supplied setup in the quotation.

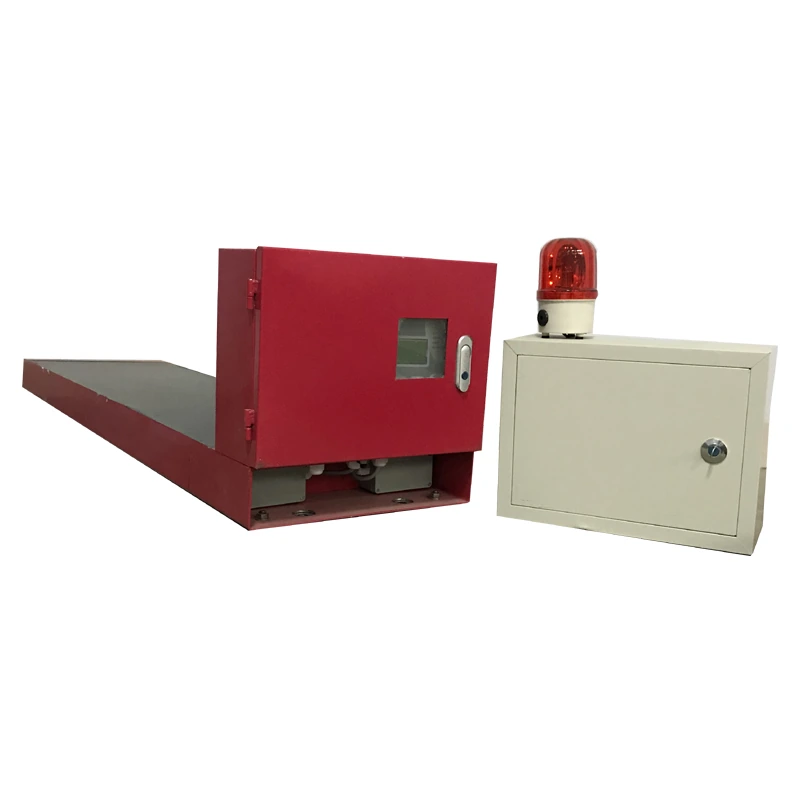
Example LJT-H sensor and electronic-control arrangement. We choose the sensor form from your conveyor profile.

Another LJT-H configuration example. The final setup follows the conveyor profile and installation space.

Example product-family control arrangement. We confirm the control unit, outputs and required connections in the quotation.
Start with the belt profile. The sensor should match the conveyor shape and the space available below the belt. We confirm the final choice from the conveyor photo or drawing.

| Selection Point | Flat-Type Sensor | V-Type Sensor |
|---|---|---|
| Main starting point | Flat conveyor profile. | Troughed or V-shaped conveyor profile. |
| What we check | Available area below the flat belt and nearby conveyor structure. | Trough shape, belt profile and available area below the conveyor. |
| What to send | Belt width plus a side/front photo or drawing. | Belt width, trough profile plus a side/front photo or drawing. |
| Final choice | Confirmed after we review the actual conveyor layout. We do not claim one sensor form is more sensitive than the other without a defined test. | |
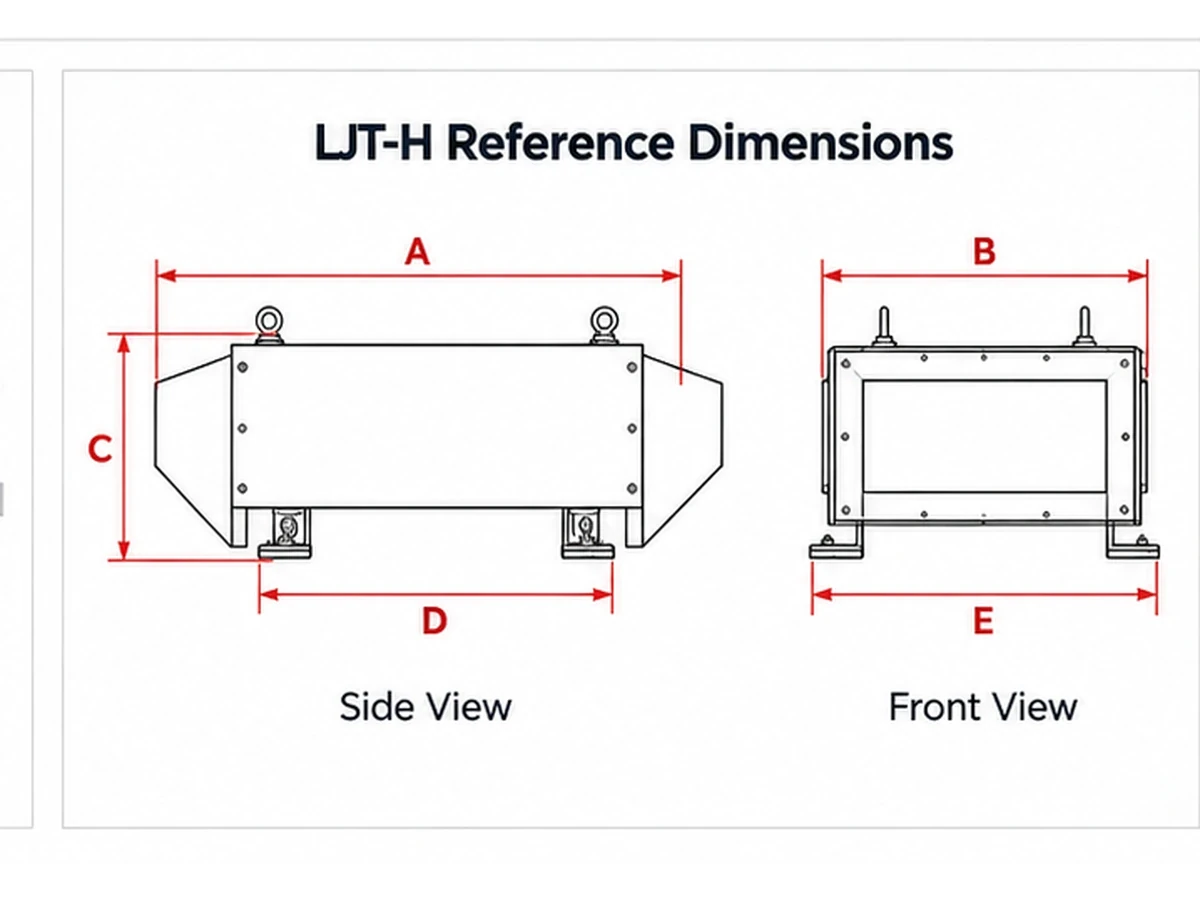
Start with conveyor belt width, then check installation space, belt profile and operating conditions before confirming the model. The table below contains the confirmed LJT-H-2 data currently available for 500–1600 mm belt widths.
| Model | Belt width (mm) | Power ≤ (W) | Belt speed (m/s) | Input | D | E | A | B | C |
|---|---|---|---|---|---|---|---|---|---|
| LJT-H-2-500 | 500 | 30 | 0.5–4.5 | AC 220 V ±10%, 50 Hz | 890 | 200 | 950 | 600 | 530 |
| LJT-H-2-650 | 650 | 30 | 0.5–4.5 | AC 220 V ±10%, 50 Hz | 990 | 200 | 1050 | 600 | 530 |
| LJT-H-2-800 | 800 | 50 | 0.5–4.5 | AC 220 V ±10%, 50 Hz | 1290 | 200 | 1350 | 600 | 530 |
| LJT-H-2-1000 | 1000 | 50 | 0.5–4.5 | AC 220 V ±10%, 50 Hz | 1390 | 200 | 1450 | 600 | 530 |
| LJT-H-2-1200 | 1200 | 50 | 0.5–4.5 | AC 220 V ±10%, 50 Hz | 1590 | 200 | 1650 | 600 | 530 |
| LJT-H-2-1400 | 1400 | 60 | 0.5–4.5 | AC 220 V ±10%, 50 Hz | 1790 | 200 | 1850 | 600 | 530 |
| LJT-H-2-1600 | 1600 | 60 | 0.5–4.5 | AC 220 V ±10%, 50 Hz | 1990 | 200 | 2050 | 600 | 530 |

This clean reference diagram is derived from the supplied LJT-H drawing and only highlights A/B/C/D/E, which are the dimensions published in the model table above. Confirm the approved project drawing before fabrication or conveyor modification.
These products solve different problems. Use the LJT-H when the main job is to detect unwanted metal and send a signal. Use magnetic separation when the main job is to capture or remove magnetically responsive material.
| Requirement | LJT-H Metal Detector | Magnetic Separator |
|---|---|---|
| Main purpose | Detect unwanted metal and send a detection signal. | Capture, separate or remove magnetically responsive material. |
| Ferrous metal | Can be detected. | Can be targeted when it is magnetically responsive. |
| Non-ferrous metal | Can be detected. | Standard magnetic separation does not target non-magnetic metal. |
| Automatic removal by the device itself | No. | Depends on the separator design and cleaning/discharge method. |
| What we need first | Target metal, belt layout, material depth, speed and required response. | Material, magnetic target, burden depth/working distance and separation point. |
The sensing element installs below the conveyor. The best position depends on the real conveyor structure, available clearance and nearby metal parts.
Choose a position where the sensor can match the belt profile and remain practical to inspect and adjust.
Show nearby idlers, beams, covers and other metal parts on the drawing or photo.
Tell us if the belt joint contains metal. An optional belt-joint detector is listed for the LJT-H family.
Send the available width, height and nearby structure if installation space is limited.
The LJT-H detects the metal and produces a signal. What happens next depends on the control design selected for the line.
The signal can be used to alert the operator when metal is detected, if this function is included in the controls.
The signal can be used as part of a conveyor-stop action when the required control connection is provided.
A marker can be used to help identify the metal location when that function is part of the selected system.
The detector signal can be integrated with a separate reject or control system when the required interface is confirmed.
If a missed metal piece could damage downstream equipment or stop production, define the target and test conditions before the final detector setup.
Record the metal type, size, shape and orientation you want to use for the test.
Use the real belt speed, material depth and metal position during the test.
Set the number of passes and the metal positions that will be checked.
Set the signal or action you expect when the detector finds the test piece.
Write down what result counts as a pass before the test is used as a performance requirement.
You do not need a perfect specification before contacting us. Start with the conveyor photo, belt width, material and target metal. We use those details to narrow the detector setup and tell you what else is needed.
We review belt width, profile, speed, material depth, nearby structure and the target metal.
We match the sensor and control setup to the conveyor layout and the response required after detection.
OEM changes are available for project requirements. We confirm the exact changes before quotation.
Installation and commissioning support is available. We confirm what support is included for the project before quotation.
We check whether the LJT-H layout matches the conveyor profile, target metal and installation position.
We identify the details that still need to be confirmed, such as material depth, splice condition, control response or a defined metal test.
We narrow the information needed to prepare the detector setup and quotation instead of asking you to complete a long specification first.
An underbelt conveyor metal detector is a conveyor belt metal detector with the sensing element below the belt. It checks conveyed material for unwanted metal as the belt moves through the detection area. The LJT-H is this type of under-belt detector.
The LJT-H detects ferrous and non-ferrous tramp metal. Actual detection still depends on the metal size and position, material depth, belt speed, belt profile and sensor setup. Define a test target when a specific minimum metal size matters.
Confirmed LJT-H-2 models on this page cover 500, 650, 800, 1000, 1200, 1400 and 1600 mm belt widths.
The confirmed model table lists 0.5–4.5 m/s. Use the actual operating speed when defining a detection test.
Start with the conveyor profile. A flat-type sensor is the starting point for a flat profile, while a V-type sensor follows a troughed or V-shaped profile. We confirm the final choice from the conveyor layout.
No. The LJT-H detects metal but does not remove it by itself. If the main job is continuous magnetic removal, a magnetic separator may be the better product family.
It can be used for control actions such as an alarm or conveyor stop when the required control function and connection are included. Tell us what the line should do after detection.
A belt joint that contains metal needs review because it can affect detection. Send the splice type plus a photo or drawing if available. An optional belt-joint detector is listed for the LJT-H family.
The main factors are the target metal, its position, material depth, belt speed, belt profile and the installation area around the sensor. A critical target should be checked under defined conveyor conditions.
Start with the material, target metal, belt width, belt profile and a conveyor photo or drawing. If available, also send belt speed, material depth, splice details and what should happen after detection. You do not need a complete specification to start.

You do not need every technical detail before contacting us. Send the conveyor photo, material, belt width and target metal first. We can identify the remaining points needed for model selection and quotation.