Corvelan Metal Inspection Equipment

LJT-F Conveyor Belt Metal Detector

Inline metal inspection for products moving on a conveyor. The LJT-F checks for ferrous, non-ferrous and stainless-steel contamination and can work with an alarm, belt stop, marking or reject device.

Best ForPackaged or unpackaged products moving on a stable conveyor
TargetFerrous, non-ferrous and stainless-steel contamination
InstallationConveyor line with a detector opening around the belt
What We Need to CheckYour product size, detector opening, line speed, packaging and what should happen when metal is found
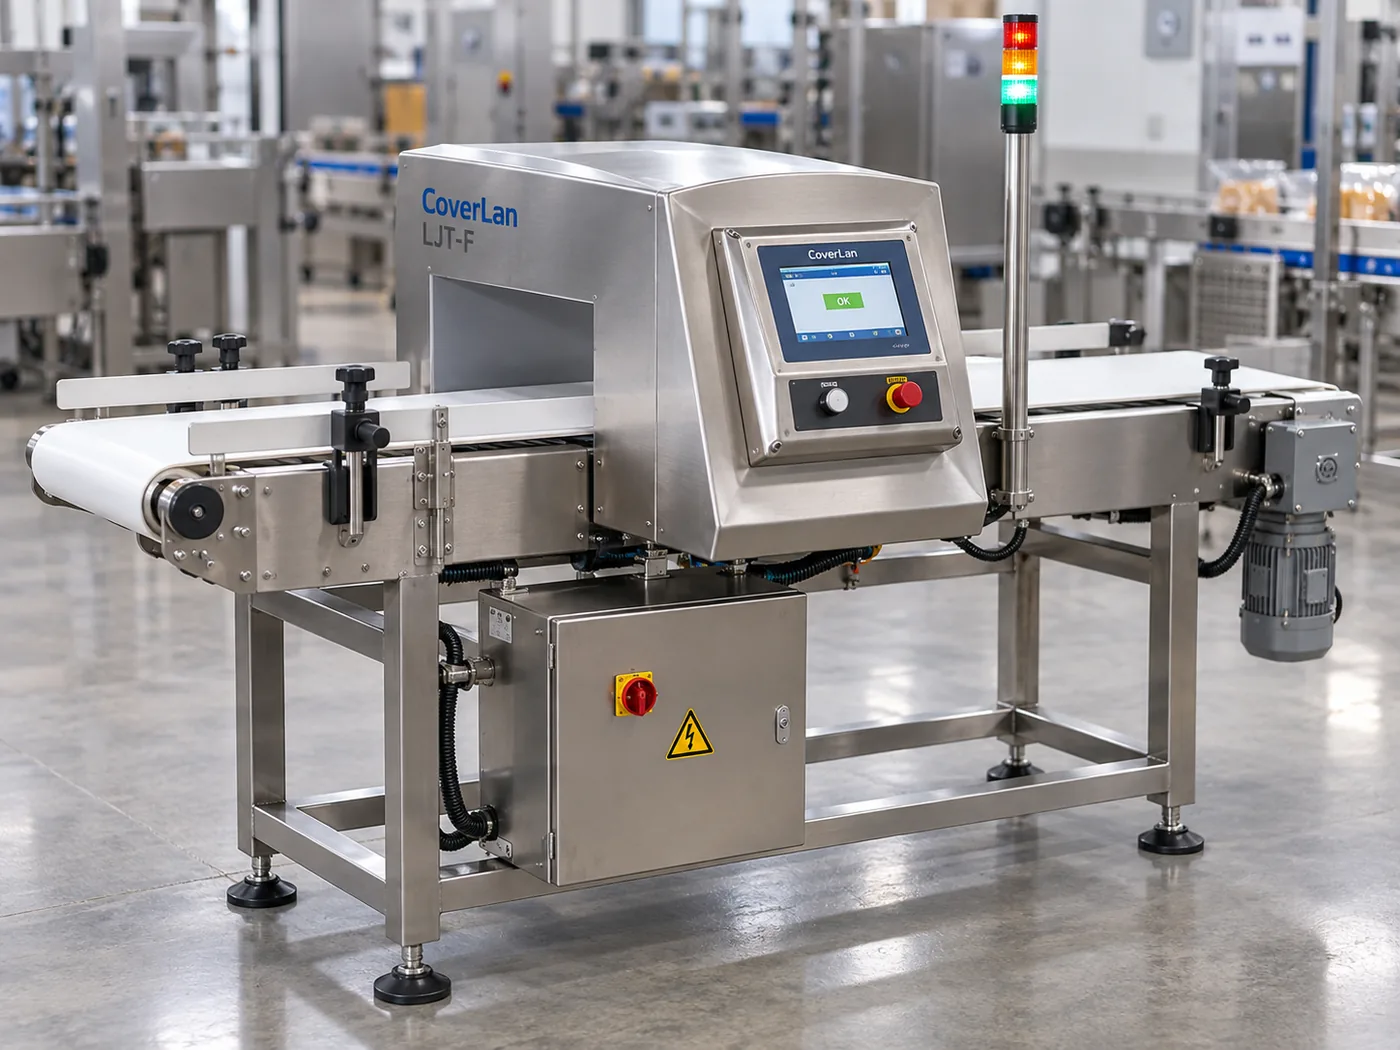
Coverlan LJT-F conveyor belt metal detector in an industrial production environment
Generated configuration visualization; final machine details depend on the confirmed project scope.
Quick Specifications

Quick LJT-F Size and Line Snapshot

Use these listed values for an early fit check. Final dimensions, operating conditions and project interfaces are confirmed for the selected model before production.

Listed Belt Width

500–700 mm

Choose around your product width and required side clearance.

Detector Opening Height

100–300 mm

Use the smallest practical opening that lets your product pass safely.

Conveyor Length

1500–1800 mm

Check available infeed, detector and outfeed space on your line.

Conveyor Height

710 mm listed

Confirm the final line interface before production.

Belt Speed

Adjustable, up to 60 m/min listed

Final speed depends on product spacing, detection requirement and response timing.

Project Fit

OEM supported

Send product size and line layout when the listed sizes do not fit your installation.

Quick Fit

Is the LJT-F Suitable for Your Line?

The LJT-F works well when your product moves on a conveyor and can pass through the detector opening. This opening is often called the detection aperture. When metal is found, the system can trigger an alarm, stop the belt, mark the product or work with an automatic reject device.

Good Fit

  • Your product moves on a conveyor and fits through the detector opening.
  • You can test the required metal size with your actual product or a representative sample.
  • Products pass through the detector in a stable position, with enough space after the detector for the required response.
  • You know what should happen when metal is found: alarm, belt stop, marking or reject.

Check These Conditions First

  • Wet, salty or electrically conductive products can create their own signal. This is called product effect.
  • Metallized or foil packaging can interfere with normal metal detection.
  • High vibration or nearby metal structures can affect a stable signal.
  • Washdown, food-contact, hygiene or other compliance requirements need to be confirmed before the final machine setup.
  • High speed or irregular product spacing can make the reject timing harder to control.

Consider Another Route

If the main contaminant is not metal—such as glass, stone, bone or dense plastic—or your product cannot pass through a practical detector opening, another inspection method or line layout may be a better fit.

Choose the Right Method

Metal Detector or Magnetic Separator — Which Does Your Line Need?

They solve different problems. A conveyor metal detector checks a moving product for metal and sends a signal when metal is found. A magnetic separator physically captures magnetically responsive contamination from the material flow.

MethodMain JobTypical Metal TargetWhat Happens After Detection or Capture
Conveyor Metal DetectorInspects product passing through a detector opening.Ferrous, non-ferrous and stainless steel under suitable product and line conditions.Can trigger an alarm, belt stop, marking or the confirmed reject device.
Magnetic SeparatorCaptures or separates magnetically responsive metal from the product stream.Mainly ferrous and other strongly magnetic contamination, depending on the separator and process.The magnetic system physically holds or diverts the captured material.
Start with your goal: if you need to inspect a finished or moving product for metal, start with metal detection. If you need to physically remove magnetic contamination from the process stream, a magnetic separator may be the better route.
Detection Objective

What Does the LJT-F Detect?

The supplied LJT-F specification groups metal targets into ferrous (Fe), non-ferrous (NFe) and stainless steel (SUS). The smallest detectable metal size is not one fixed number for every product. It depends on your product, detector opening, metal type and position, line speed, packaging and the surrounding environment.

Important: do not choose the detector from a sensitivity number alone. First define the metal test piece and the test method the system needs to pass with your real product under your real line conditions.
Working Principle

How the Conveyor Metal Detection Process Works

The basic process is simple: move the product through the detector, check the signal, identify a metal-related change, then make the line respond in the agreed way.

Product Passes Through

The conveyor carries the product through the detector opening at the intended line speed.

Detector Checks the Signal

The detector monitors the signal while the product passes through the opening.

Metal Signal Is Found

If the signal reaches the set detection level, the system identifies the product for the required response.

The Line Responds

The confirmed setup can sound an alarm, stop the belt, mark the product or activate an automatic reject device.

Important: detection and line response should be checked together. A detector can find metal correctly but still remove the wrong product if product spacing and reject timing are not matched.
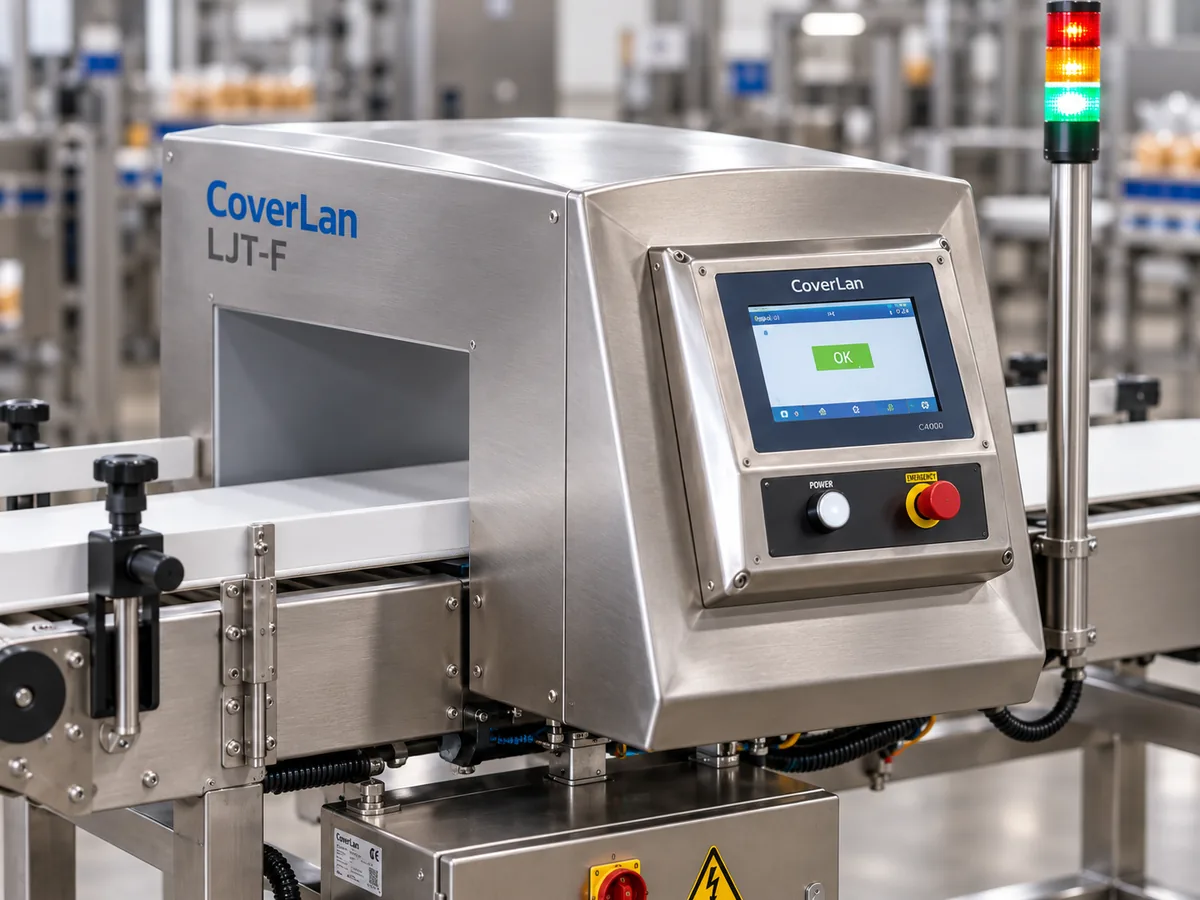
Close-up of the Coverlan LJT-F conveyor metal detector control panel and inspection tunnel
Generated equipment-detail visualization. Final controls and hardware depend on the confirmed machine setup.
Performance Factors

What Affects Metal Detection Performance?

For project review, we check the core factors used across conveyor metal-detection engineering: detector opening, product effect, metal type and position, packaging, line speed, nearby metal, vibration and response timing.

1. Detector Opening Size — Aperture

Use the smallest opening that still lets your product pass safely. A larger detection aperture usually makes very small pieces of metal harder to detect.

2. Wet or Conductive Products — Product Effect

Some products can create a signal even when no metal is present. Moisture, salt, temperature and product consistency can change this signal. The industry calls this product effect, and it can make very small metal pieces harder to detect.

3. Metal Type and Position

Different metals are not equally easy to detect. Ferrous metal, non-ferrous metal and stainless steel can produce different detector responses. The size, position and direction of the metal piece also matter.

4. Belt Speed and Product Spacing

The supplied specification lists an adjustable belt speed up to 60 m/min. The final speed still needs to work with your product spacing, required metal detection level and reject timing.

5. Alarm, Belt Stop or Reject Timing

A belt stop, also called an interlock, needs different space and controls from an automatic reject system. Fast lines also need enough distance after the detector so the correct product can be removed.

6. Installation Environment

Nearby metal, vibration and electrical noise can affect the detector. We also need enough clear space around the detector so surrounding metal parts do not interfere with it.

Troubleshooting

What Can Cause False Alarms or Unstable Detection?

Unstable results do not always mean the detector needs a higher or lower sensitivity setting. First check the product, opening, surrounding metal and line conditions.

Wet, Salty or Conductive Product

The product can create its own signal. This product effect can make small metal harder to separate from the normal product signal.

Detector Opening Larger Than Needed

A larger unused opening generally makes very small metal harder to detect. Start with the smallest practical opening for your product.

Nearby or Moving Metal

Metal close to the detector can interact with the sensing field. Keep a clear metal-free area around the detector as required by the final installation.

Vibration or Electrical Noise

Machine vibration, unstable mounting or electrical interference can disturb a stable signal and should be checked during installation.

Packaging or Product Changes

Conductive packaging, product temperature, moisture or recipe changes can change the normal product signal.

Spacing and Reject Timing

If products are too close together or spacing changes, the detector may find metal correctly but the reject timing can remove the wrong item.

Seeing unstable detection? Send us your product, detector opening, belt speed, product spacing, packaging and surrounding line layout before changing the detection setting.
Selection Path

How to Start Selecting an LJT-F

You do not need every technical detail before the first review. Start with the product, detector opening, line speed and required response, then confirm the remaining items step by step.

Check Your Product Size

Confirm the maximum product width, height and length. The product needs to pass through the detector opening without touching it.

Choose the Smallest Practical Opening

Use the smallest detector opening that still lets the product pass safely. A larger unused opening can make very small metal harder to detect.

Check Product Effect

Wet, salty or electrically conductive products can create their own signal. This is called product effect and should be checked with the actual product.

Check Speed and Product Spacing

Line speed needs to be considered together with product length, spacing, response distance and the time needed for a stop or reject action.

Choose the Line Response

Decide whether the line should alarm, stop, mark the product or use an approved automatic reject device after metal is found.

Confirm With Product Testing

Final detection performance should be checked with the actual product or a representative sample under the intended line conditions.

Check Before Final Selection

When We Need More Information Before Selecting a Detector

Some line conditions need a closer review before we confirm the model or detection target. Sending these details early helps avoid choosing a detector opening, response method or test condition that does not match the real process.

Product and Packaging Conditions

  • Metallized or foil packaging
  • Highly conductive product
  • Very wet or salty product
  • Large variation in product temperature, moisture or formulation

Line and Installation Conditions

  • Very high line speed or irregular product spacing
  • Very large detector opening
  • Very short distance available for belt stop or reject action
  • Existing metal structure, vibration or electrical equipment close to the detector
Fixed sensitivity requirement? Send the required metal type, test-piece size, product condition, detector opening and intended line speed before final model selection.
Model Sizes

LJT-F Sizes and Conveyor Dimensions

The table below shows the dimensions listed in the current LJT-F specification. Start with your maximum product width and height, then check conveyor length and line height against the available installation space.

How to use this table: 1) find the smallest detector opening that lets the product pass safely; 2) check belt width against product width; 3) check conveyor length and height against your line; 4) send the layout to us if a listed size does not fit.
ModelNominal Belt WidthDetector Opening HeightDetector Belt WidthConveyor LengthConveyor HeightGood Starting Point When…
LJT-F-5010500 mm100 mm470 mm1500 mm710 mm
LJT-F-5020500 mm200 mm470 mm1500 mm710 mm
LJT-F-6015600 mm150 mm570 mm1500 mm710 mm
LJTF-6020600 mm200 mm570 mm1600 mm710 mm
LJT-F-7030700 mm300 mm670 mm1800 mm710 mm

The supplied specification also lists 8 memory entries and an adjustable belt speed up to 60 m/min.

Need a different size? Corvelan supports OEM configurations for project-specific requirements. Send us your product size, line layout and required detector opening so we can review a suitable machine setup.
Choose a Setup

How to Choose the Right LJT-F Setup

What to CheckWhy It MattersWhat to Send Us
Your product and packagingWet, salty or conductive products and some packaging can affect the detector signal and product handling.Product name, product condition, moisture or salt condition, and packaging type.
Product sizeHelps us choose the smallest detector opening that still passes your product safely.Maximum product width, height and length.
Metal you need to detectTells us what metal test piece and test method need to be considered.Fe, non-ferrous metal or stainless steel, plus the required test-piece size if you already have one.
Line speed and outputOutput, often called throughput, means how much product passes through the line in a set time. It affects spacing and how much time the line has to respond.Current belt speed, target output or throughput, and product spacing.
Available spaceTells us whether the conveyor length, line height and detector position can fit your line.Line drawing, available space, and infeed and outfeed details.
What should happen after detectionDefines how the line should respond when metal is found.Alarm, belt stop or interlock, marking, or automatic reject preference.
How you want to test the systemGives us a clear test method before any sensitivity result is discussed.Test-piece standard, test positions, repeat count, and pass/fail requirement if you already have one.
Line Response

What Should Happen When Metal Is Detected?

Detection is only useful when the line response matches your product and production flow. The supplied information lists alarm, belt stop or interlock, marking and automatic rejection as available response routes; the final hardware and sequence are confirmed for each project.

ResponseWhat It DoesWhat We Need to Check
AlarmAlerts the operator when metal is detected.Alarm type and what the operator should do next.
Belt Stop / InterlockStops product movement or sends a stop signal to the line.Stop logic, restart procedure and upstream/downstream line behavior.
MarkingIdentifies the suspect product for later removal or checking.Product surface, package type and marking method.
Automatic RejectRemoves the suspect product from the production line automatically.Product weight, size, spacing, belt speed and available reject distance.
OEM Line Fit

Need an LJT-F Setup for an Existing Conveyor?

Corvelan supports OEM configurations for project-specific line requirements. Start with your product size, required detector opening, conveyor height, available line length and the response you need after metal is found.

Machine Fit

We review detector opening, conveyor width, conveyor length and line height against your product and available installation space.

Line Interface

Send a drawing or clear layout showing infeed, outfeed, product direction, nearby metalwork and where the line needs to stop, alarm, mark or reject.

OEM support does not mean every material, control, enclosure or compliance option is automatically available. Project-specific requirements are confirmed before quotation and production.

Installation Support

Installation and Commissioning Support

Before we prepare the final machine setup and quotation, send us the infeed and outfeed heights, available conveyor length, product transfer details, detector opening, product guides, line direction, nearby metalwork and access for cleaning and maintenance. If you need automatic rejection, also send product spacing, available reject distance and any air or electrical requirements.

Corvelan can provide installation and commissioning support for supplied equipment. Commissioning means checking the machine setup and operation after installation. The exact support scope is confirmed for each project.

If your line has washdown, food-contact or other compliance requirements, tell us which materials, documents and cleaning method you need. Food-processing use alone does not prove food-contact or certification status.
Maintenance & Safety

Keep the Detector Area Clean and Stable

Keep the conveyor and detector opening free from buildup and loose metal that can cause false signals or unstable operation. Routine checks should include belt tracking, detector mounting, changes to nearby metal, reject-device movement and any sensor used to confirm a rejected product.

Electrical isolation, guarding and access procedures should follow the final machine design and your site safety rules.

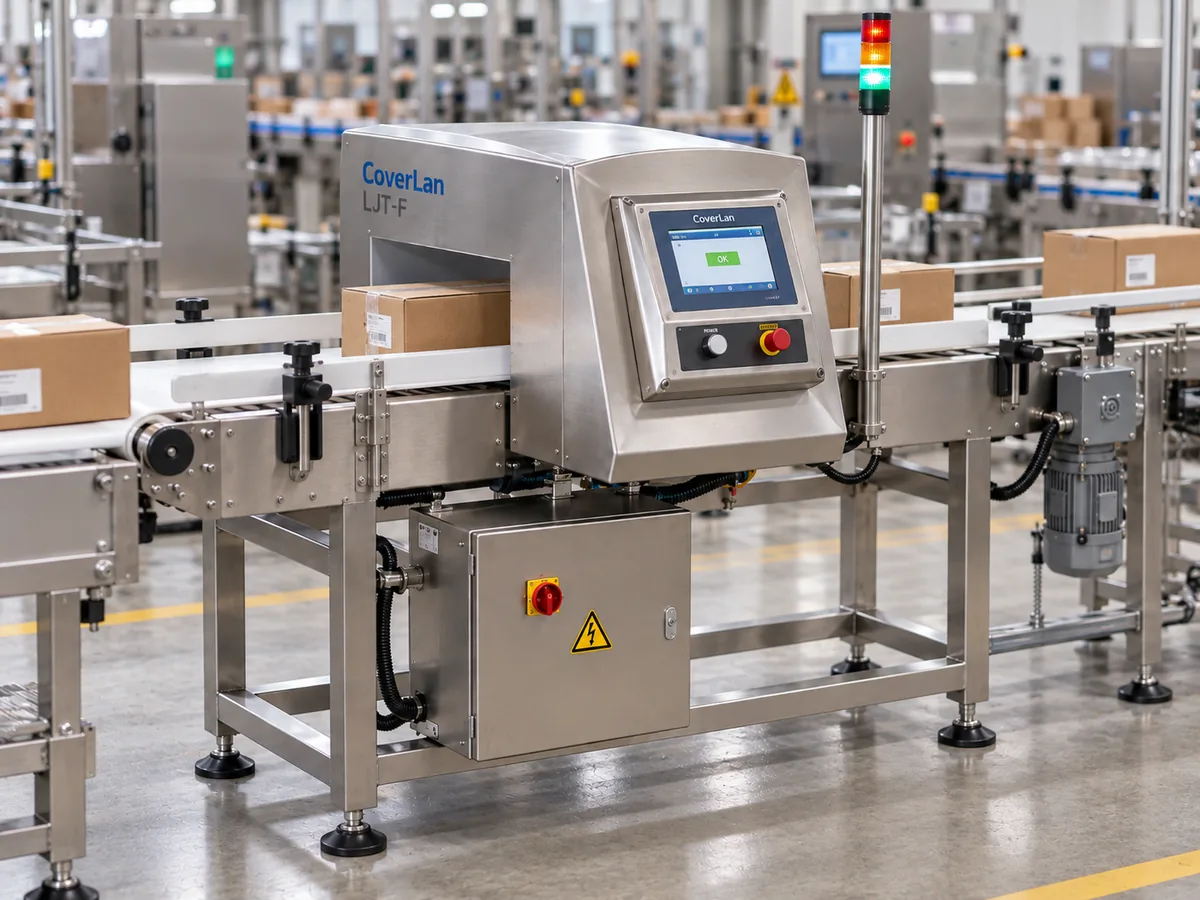
Coverlan LJT-F conveyor metal detector integrated into a packaging production line
Generated application visualization showing a representative conveyor-line integration; not a verified customer-site photograph.
Test the System

How Do You Check That the Detector Works?

A proper detection test should show that the complete system works under your real line conditions. This type of check is often called validation. Use your actual product or a representative sample, agreed metal test pieces and the intended belt speed. Place the test pieces in the positions you need to check and confirm the full response from detection through alarm, belt stop or rejection.

Before testing, define the metal size the system needs to detect and what the line should do when that metal is found. If you already have a retailer, customer or internal QA test method, send it with your inquiry so we can review the machine setup against it.

How We Work

Why Corvelan for LJT-F Projects?

We focus on matching the detector to the product and production line instead of choosing a machine from one number alone.

Start With Your Product

We review product size, condition, packaging and the metal you need to detect before narrowing the detector opening and model.

Check the Full Line

Line speed, product spacing, available space and the required alarm, stop, marking or reject response are considered together.

OEM Line Fit

OEM configurations can be reviewed when the listed dimensions do not match your existing conveyor or installation space.

Installation and Commissioning Support

Support is available for supplied equipment, with the project scope confirmed before delivery.

Define the Detection Check

We recommend confirming the product, test piece, detector opening, speed and required response before treating a sensitivity result as meaningful.

Keep the Unknowns Visible

If a condition still needs testing or confirmation, we keep it open instead of turning an unverified assumption into a fixed performance claim.

Next Steps

What Happens After You Send the Line Details?

1. Before Quotation

We check the product, maximum size, line speed, detector opening, available space and what the line should do when metal is found.

2. Before Production

We confirm the selected model or OEM direction, final dimensions, machine interfaces, project drawing or specification, and agreed options.

3. Before Startup

We confirm the installation condition, product setup, detection test method and required alarm, stop, marking or reject response.

For a Quote

What to Send Us for a Quotation

Start with four items. These are usually enough for us to check the basic machine size and line setup without asking you to complete a long technical form.

Your Product

Tell us what moves on the conveyor, how it is packed, and the maximum product dimensions.

Metal You Need to Detect

Tell us whether you need to detect Fe, non-ferrous metal or stainless steel, plus any required test-piece size.

Line Speed and Output

Send the belt speed, product spacing and target output. Output is also called throughput.

Available Space and Line Layout

Send the available space, line height, infeed and outfeed arrangement, and what you want the line to do after metal is found.

If available, also send the moisture or salt condition, temperature, line drawing, cleaning requirement, power details, reject preference, destination and any required test or documentation standard.

FAQ

LJT-F Conveyor Belt Metal Detector FAQ

What metals can a conveyor belt metal detector detect?

The LJT-F specification uses ferrous, non-ferrous and stainless-steel categories. The smallest detectable metal size still depends on the product, detector opening, metal position, packaging and line conditions.

How do I choose the detector opening size?

Start with the smallest opening that lets your product pass safely. A larger opening generally makes very small metal harder to detect, so send the maximum product width and height before the final model is selected.

Why does metal-detection sensitivity vary?

Sensitivity changes with detector opening, metal type and position, product characteristics, packaging, line speed, vibration, nearby metal and other operating conditions. This is why one sensitivity number should not be treated as a guarantee for every product.

What is product effect in metal detection?

Wet, salty or electrically conductive products can create their own signal inside a metal detector. The industry calls this product effect. It can make small metal harder to separate from the normal product signal and can contribute to false rejects if the setup is not matched to the product.

What can cause false alarms or unstable detection?

Common causes include product effect, an opening larger than needed, nearby or moving metal, vibration, electrical interference, conductive packaging, product changes, unstable spacing and incorrect reject timing.

Can the LJT-F stop or reject product automatically?

The supplied information lists alarm, belt stop or interlock, marking and automatic rejection as available response routes. The final response hardware and timing need to match the product, spacing, belt speed and available line space.

Do I need a metal detector or a magnetic separator?

Use a metal detector when you need to inspect a moving product for metal and trigger a line response. Use a magnetic separator when the main job is to physically capture magnetically responsive contamination from the process stream.

What should I send Corvelan for selection and quotation?

Send the product and packaging, maximum product dimensions, metal or test-piece requirement, belt speed or output, product spacing, available line space and the response you want after metal is found. A line drawing is useful when available.

Send Your Detection Requirement

Share your product, maximum size, metal target, line speed or output, available space and required line response. We will check the LJT-F size, OEM direction if needed, and the details that still need to be confirmed.

Get An Instant Quotation Now