
Measure the Distance to the Hardest Iron Piece
Do not measure only the empty space above the material. Measure from the magnet face to the iron piece that is hardest to reach inside the material.
Find equipment by installation point and separation task.
All magnetic separators →Start with the material or production line you need to protect.
All applications →Compare technologies, check parameters and prepare your RFQ.
All guides →See the factory, quality checks and answers before you request a quotation.
Oil-Cooled Conveyor Iron Removal
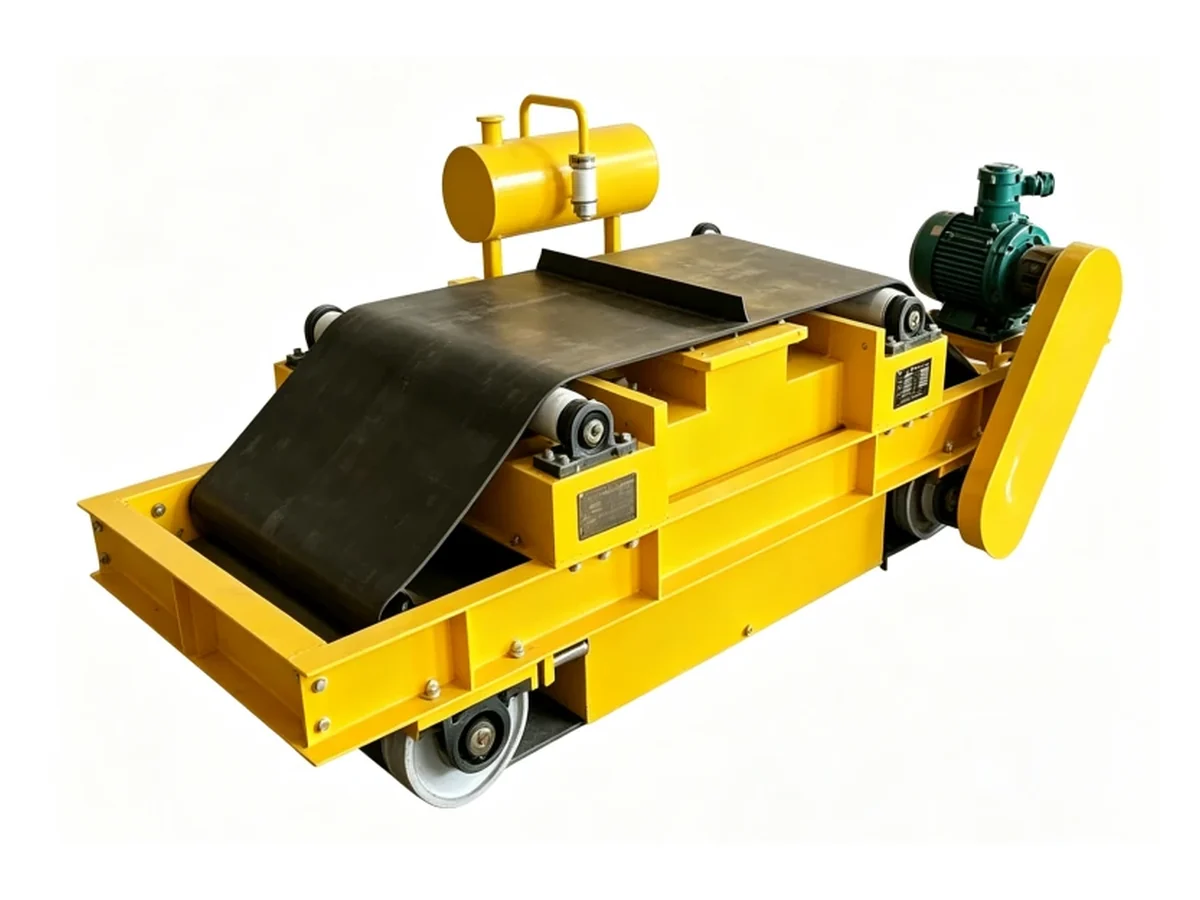
Use this Corvelan separator on dry conveyor lines that regularly carry unwanted iron or steel. These unwanted pieces are often called tramp iron. A moving cleaning belt removes the captured metal automatically.
We do not choose the separator from conveyor width alone. The key distance is from the magnet face to the iron piece that is hardest to reach. We call this the working distance.
Quick Engineering Answers
Start with the operating condition, not the product name. These quick rules show which separator type to check first.
Quick Fit
Choose this separator when your process is dry, conveyor-fed and needs to remove iron or responsive steel. It fits best when the metal appears often enough to make manual cleaning disruptive. Use another option if your process does not match these conditions.
Use self-unloading when iron appears often and production should keep running. We then size the magnetic reach for the real material depth and target position.
Use a manual-clean suspended magnet when iron appears only occasionally. Choose it only when planned stops are acceptable and the magnet can be cleaned safely.
Use another separator for aluminum or copper, liquid or slurry processes, or fine weakly magnetic mineral recovery.
Choose the Right Separator
Choose the separator type from the real operating condition first. Then choose the exact machine size. The table shows what to use and what information to send us.
| Your Situation | Use This | Avoid This | What to Send Us |
|---|---|---|---|
| Iron appears often and the line should keep running | Oil-cooled self-unloading electromagnet | Manual cleaning as the normal method | Belt speed, material depth, target iron, iron frequency, discharge side and collection area. |
| Iron appears only occasionally and planned stops are acceptable | Manual-clean suspended magnet | Automatic cleaning when the process does not need it | Target iron, safe cleaning access and the normal stop schedule. |
| Material is shallow, belt speed is moderate and iron is easy to catch | Compare a suspended permanent magnet first | Electromagnet without a reach or duty reason | Working distance, target iron and belt speed. |
| Material layer is deep | Electromagnetic separator | Choosing from conveyor width or air gap alone | Maximum normal material depth and the deepest target position. |
| Belt speed is high | Electromagnetic separator + capture test | Using a static pickup test as the only check | Belt speed, working distance and the iron piece that must be removed. |
| Material is deep and belt speed is high | Electromagnetic separator + capture test | Choosing the final machine from a catalog table alone | Maximum material depth, belt speed, target iron and target position. |
| Small important iron can sit at the bottom | Electromagnetic separator with enough magnetic reach | Testing only the largest and easiest piece | Smallest required iron, bottom position and real working distance. |
| Iron pieces are large or heavy | Heavy-duty electromagnetic separator | Choosing from magnet-face Gauss alone | Iron size, shape, mass, position and discharge path. |
| A lot of iron arrives frequently | Self-unloading separator | Checking magnetic pickup without checking discharge | Iron frequency, iron amount, chute, bin and collection space. |
| Iron is sharp or highly abrasive | Protected or heavy-duty cleaning belt | Standard belt without an impact check | Iron photos, shape, mass, impact path and discharge drop. |
| Electromagnet runs long hours or under demanding duty | Oil-cooled electromagnet | Choosing cooling from the product name alone | Operating hours, ambient condition, dust, moisture and service access. |
| The site does not allow an oil-filled cooling system | Air-cooled electromagnet | Oil-cooled electromagnet | Operating hours, ambient condition, airflow and service space. |
| No electrical supply is available, or the site wants the simplest magnetic source | Suspended permanent magnet if it reaches the target | Electromagnet unless reach or duty requires it | Working distance, target iron and belt speed. |
| Aluminum or copper is the main unwanted metal | Eddy-current or other non-ferrous separator | Suspended electromagnet as the main separator | Metal type, particle size and how it appears in the product. |
| The process is liquid or slurry | Wet magnetic separator | Dry-belt suspended separator | Slurry details, solids content, particle size and separation goal. |
| The goal is fine weakly magnetic mineral recovery | High-intensity or high-gradient separator | Standard tramp-iron electromagnet | Mineral sample, particle size and required separation result. |
| Stainless steel is the target | Test the actual grade and condition | Assuming all stainless responds the same way | A real sample, grade if known, size and process condition. |
| There is no side space for cross-belt discharge | Change discharge direction, location or separator type | Standard cross-discharge layout | Side-view drawing, available space and the planned collection point. |
| The existing conveyor has low headroom | Check the general arrangement (GA) drawing first | Choosing the magnet before checking space | Headroom, material depth, support steel and maintenance space. |
| This is a new conveyor line | Reserve separator space during conveyor design | Adding the separator after the steelwork is fixed | Conveyor GA, support position, headroom, chute and collection area. |
| This is an existing-line retrofit | Check the existing conveyor first | Copying a new-line layout | Headroom, nearby steel, support, power, service access and discharge space. |
| The area is hazardous or explosive | Dedicated certified hazardous-area design | Standard separator setup | Area classification and the required certification scope. |
| This is a food or hygienic process | Dedicated hygienic or food-compatible design | Standard mining or aggregate setup | Contact materials, cleaning method and required certifications. |
Example Selection
This configuration example shows how iron frequency, conveyor conditions and cleaning requirements affect equipment selection.
Choose an oil-cooled self-unloading electromagnet. Frequent iron makes repeated manual cleaning a production problem, so automatic discharge becomes part of the machine choice.
The line should not stop several times each shift just to clean the magnet.
Working distance, iron amount, belt running, discharge direction and the collection area.
Conveyor data, material depth, iron photos, iron frequency and the proposed installation point.
Material & Metal Fit
Use this equipment for iron or steel pieces that respond strongly to a magnet in dry bulk material on a belt conveyor. Choose the separator from the hardest metal piece you still need to remove, not from the material name alone.
Typical dry conveyor streams include ore, aggregate, coal, bulk fuel, clinker-related material, recycling feed, wood and biomass. The unwanted metal should be iron or responsive steel.
Use a non-ferrous separator for aluminum or copper. Test stainless steel using the actual grade and condition. Use another separator for slurry or weakly magnetic mineral work.
Working Principle
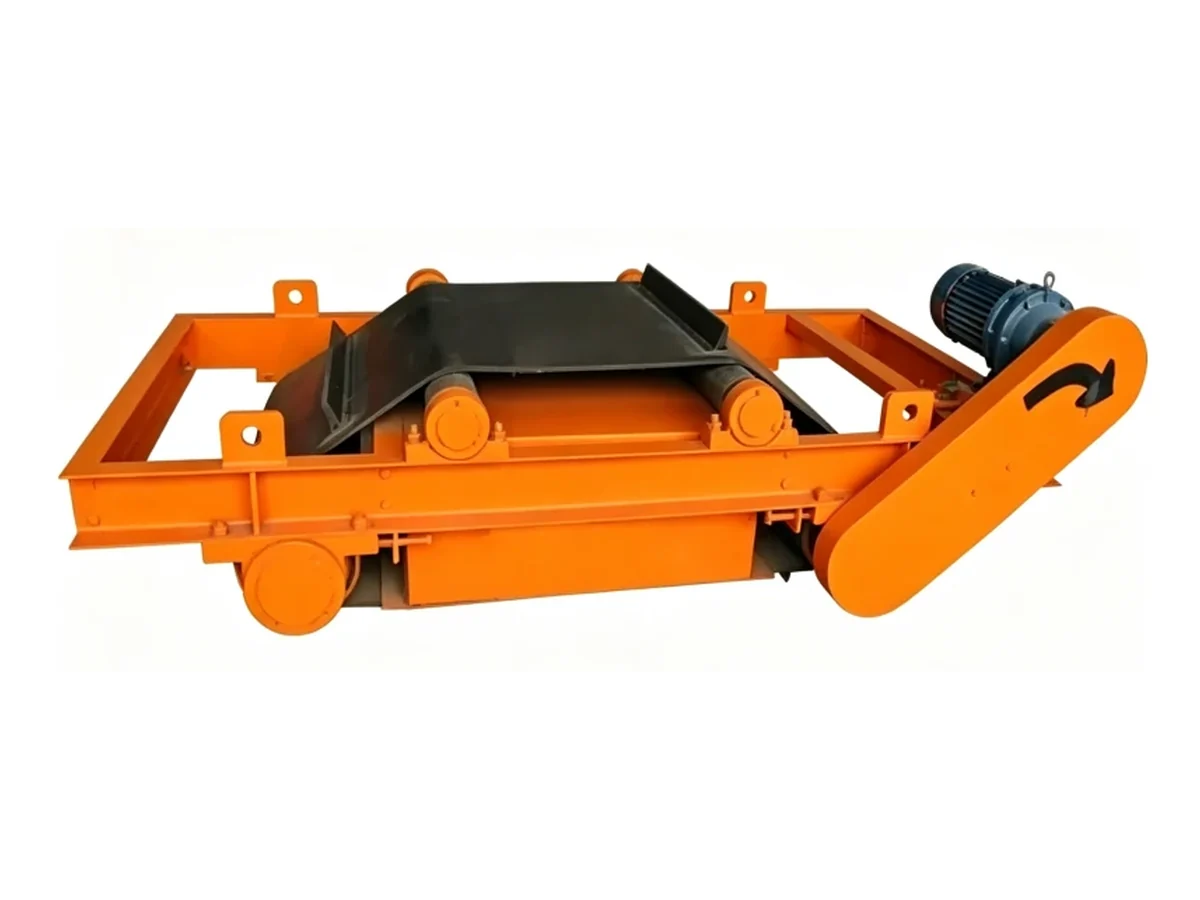
The energized coil creates a magnetic field above the conveyor. Iron or steel is pulled from the material toward the magnet. A driven cleaning belt carries the metal out of the strong magnetic zone, where it drops into the collection area. Oil cooling carries heat away from the electromagnetic assembly.
The conveyor carries the material under the suspended magnet. The material layer on the belt is often called the burden.
The magnetic field must be strong enough at the iron position to pull the piece from the moving material.
The cleaning belt moves captured metal away from the product stream.
After the metal leaves the strong magnetic zone, it drops into the chute, bin or other collection area.
What Affects Capture
Start with the real working distance. Then check material depth, belt speed, iron size and position, how much iron appears and nearby steel. Do not choose the separator from belt width or magnet-face Gauss alone.
Do not measure only the empty space above the material. Measure from the magnet face to the iron piece that is hardest to reach inside the material.
Do not use the average material depth if the conveyor regularly runs deeper. Use the deepest normal layer the separator must protect. Engineers often call this burden depth.
As belt speed rises, the magnet has less time to pull the iron out. For fast belts, test the required iron at a similar speed and working distance.
Define the smallest required piece, typical piece, largest or heaviest piece, and the deepest position that still needs protection.
If captured metal builds up faster than the cleaning system removes it, the belt, chute or bin becomes the bottleneck.
Show us support steel, chutes, guards and rollers near the magnet. Move or redesign steel that blocks the magnetic zone or service access.
Example Selection
This example shows the selection method. The numbers are not Corvelan model ratings or a published customer result.
Use an electromagnetic separator and run a capture test at the real working distance. Deep material moves the iron farther from the magnet, while a fast belt gives the magnet less time to catch it.
Use the required iron piece at the agreed distance and a movement condition close to the real belt speed.
Move the magnet closer, reduce material depth, use a stronger setup, change the installation point or change separator type.
Do not replace the real test with an easy plate placed close to the magnet just to get a pass.
Choose the Magnetic and Cooling Type
Choose the magnetic and cooling type from running duty, required reach and site limits. Do not choose from the product name alone.
Choose oil-cooled when the electromagnet runs for long periods or works under demanding duty. It is also the first option to review for deep material or longer magnetic reach when oil cooling fits the site.
Choose air-cooled when you still need an electromagnet but do not want an oil-filled cooling system. The selected design must still handle the required duty and site conditions.
Choose a permanent magnet when it can catch the required iron at the working distance without electrical power. If it can do the job, there is no reason to add an electromagnet only for complexity.
Oil cooling manages heat. It does not tell you by itself how much iron the separator can catch. Magnetic performance still depends on the coil, magnetic circuit, working distance and the iron you need to remove.
Choose the Cleaning Method
Choose self-unloading when iron appears often enough to make manual cleaning interrupt production. It also makes sense when access is difficult or too much metal would build up on the magnet. Choose manual cleaning only when iron is truly occasional.
How Corvelan Chooses the Final Setup
We start with the problem you need to prevent. Then we check the hardest iron piece, working distance, iron amount, magnetic and cooling type, discharge system, installation space, electrical requirements and test method. Conveyor width alone is never enough.
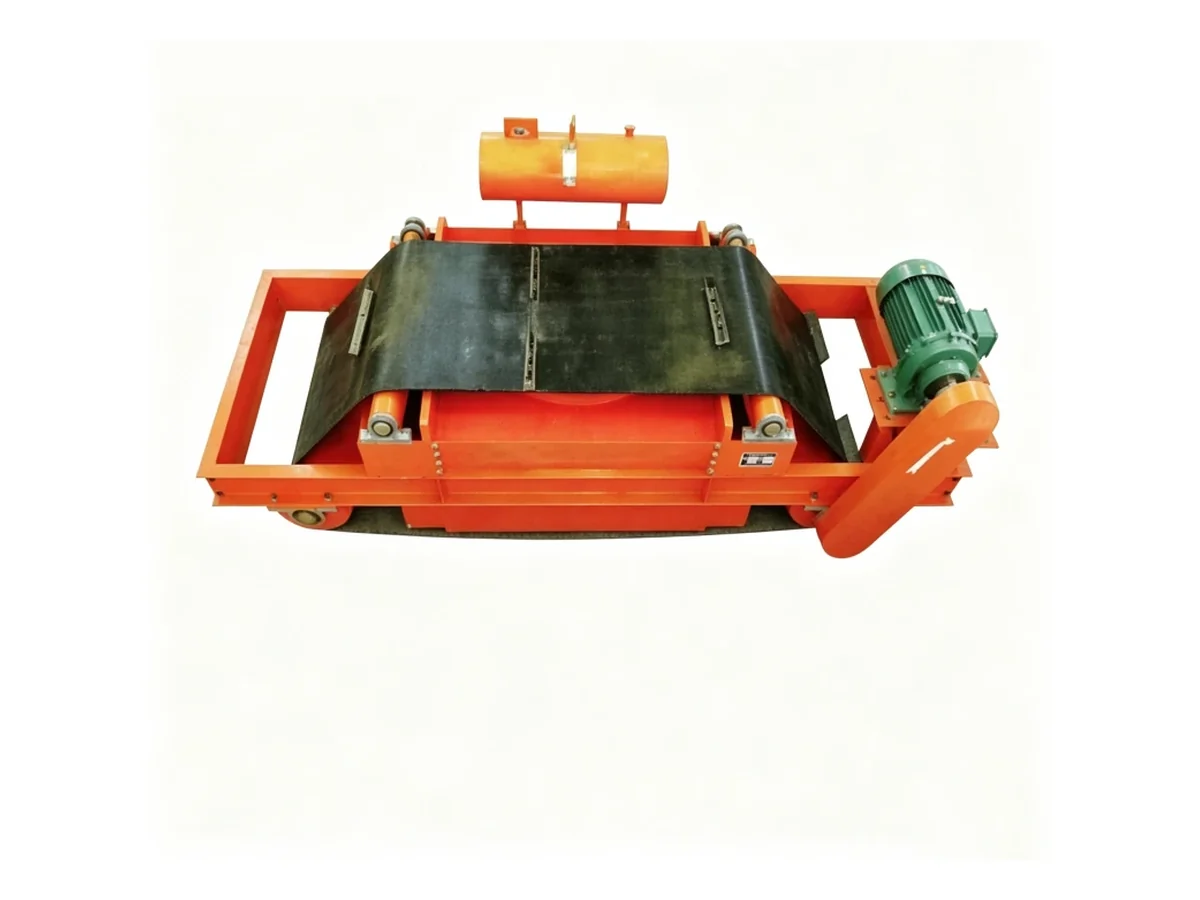
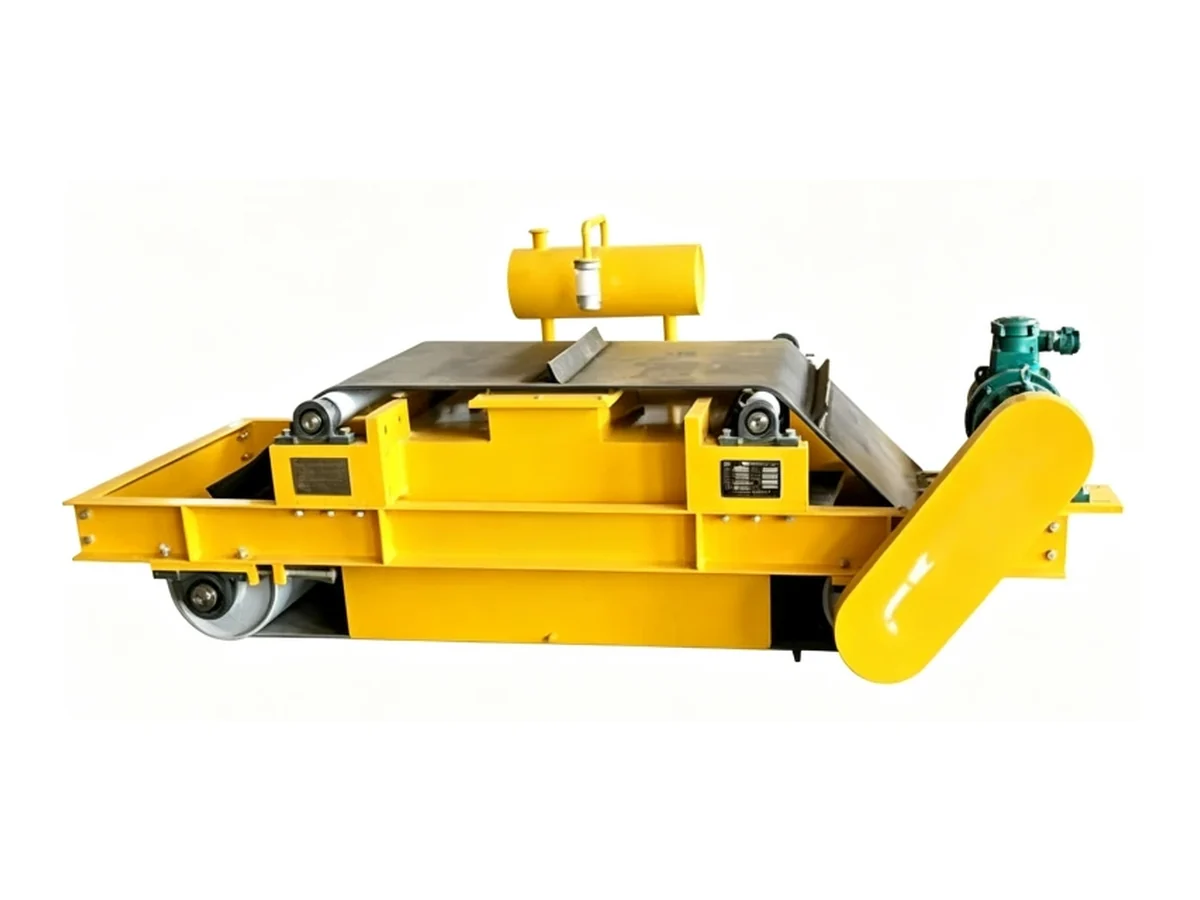
Corvelan separators can use different frames, rollers and drive layouts to match the selected size and installation. The project drawing confirms the final belt path, frame, drive side, maintenance space and suspension points.
We confirm magnetic performance, power, oil details and final dimensions in the project technical documents. Do not read these values from product photos.
What We Confirm Before Production
Do not start production until the main conveyor, magnetic, cooling, cleaning, installation and electrical details are confirmed. These items control whether the separator fits and how we check it.
| Item to Confirm | What We Confirm | Do Not Start Production If |
|---|---|---|
| Conveyor details | Belt width, belt speed, material profile, normal and maximum material depth, travel direction and separator position. | The conveyor layout or material depth is still only an estimate. |
| Iron pieces to remove | Smallest required, typical and largest or heaviest piece, plus where each piece can sit in the material. | Only the easiest visible steel piece has been checked. |
| Working distance | Magnet face to the hardest iron piece at the deepest normal material condition. | Only the empty air gap to the material surface has been measured. |
| Magnetic requirement | Agreed magnetic measurement or capture requirement at a defined condition. | The requirement is only an undefined “high Gauss” statement. |
| Oil-cooling setup | Cooling type, included parts, running duty and service access. | Oil type, oil volume or thermal limits are being guessed from photos. |
| Self-unloading system | Belt path, drive, discharge direction, protection, guards and collection area. | Captured metal has no safe place to discharge. |
| Support and clearance | Suspension points, headroom, nearby steel, maintenance space and lifting access. | The machine cannot be serviced safely. |
| Electrical and controls | Site power supply, electromagnet controls, cleaning-belt drive, interlocks and plant connections. | Voltage or control responsibility is still unclear. |
| Test method | Drawing check, dimension check, function check, magnetic measurement and/or capture test. | The pass/fail method has not been agreed. |
When You Should Choose Another Separator
Do not use this separator for a process that needs a different separation method, special certification or a different installation layout. Choose another option when any condition below applies.
Check the Installation Before You Order
Do not treat installation as a final drawing formality. Do not approve the layout until headroom, working distance, support, nearby steel, maintenance access and the metal discharge path all work together.
| What to Check | Good | If It Does Not Work |
|---|---|---|
| Headroom | Magnet, cleaning belt and support fit at the required working distance, with maintenance space. | Change the installation point, support or separator type. |
| Discharge space | Captured iron can enter the chute or bin without falling back into the product stream. | Change the discharge side, direction or collection layout. |
| Nearby steel | Support steel, chutes and guards do not block the magnetic zone or service access. | Move or redesign conflicting steel before installation. |
| Maintenance access | Drive, take-up, belt, guards and cooling or electrical service points are accessible. | Redesign the layout if routine service cannot be done safely. |
| Material clearance | The deepest normal material and normal surges do not hit the magnet or cleaning belt. | Increase clearance or control the material profile. |
| Support | The suspension and load path are shown on the project drawing. | Do not install until the responsible project team checks the support design. |
Existing Conveyor Example
This is an installation example, not a published customer project.
Check the conveyor drawing before choosing the machine size. On an existing line, headroom, nearby steel, discharge space and maintenance access can rule out a layout before magnetic size is finalized.
Move the separator, change the layout or choose a different machine arrangement before ordering.
Change the discharge direction, move the separation point or use another separator layout.
Change the support layout before the machine is approved for installation.
Cleaning, Maintenance & Safety
Check the cleaning belt, drive, electrical system, oil-cooling parts and suspension separately. Stop the machine if the belt tracks badly, the drive is abnormal or oil leaks. Also stop for damaged electrical parts or unsafe suspension.
Check belt tracking, tension, wear, scraper or cleat condition, pulleys, bearings, drive, guards and the full metal path.
Check oil-cooling parts, connections, enclosure and electrical components for leaks, unusual heat, dirt or damage.
Check suspension points, fasteners, guards, clearance and material buildup. Do not run with damaged suspension or blocked discharge.
Before Shipment
We agree the required checks before production starts. If the order includes a magnetic value or capture test, the test position, distance, target and pass condition are defined before the test.
Check the main dimensions, suspension points, discharge direction and other project dimensions against the approved drawing.
Run the belt and check direction, tracking, drive operation and the path used to discharge captured iron.
If a magnetic value is part of the order, define the test point and distance first. Record the result at that same position.
For difficult jobs, use the agreed iron piece at the agreed distance. Use a moving test when belt speed is part of the problem.
Check the machine setup, electrical information, visible assembly and any test records included in the order before packing.
Write down the iron piece, target position, working distance, material condition, movement condition and what counts as a pass.
Actual Corvelan Product
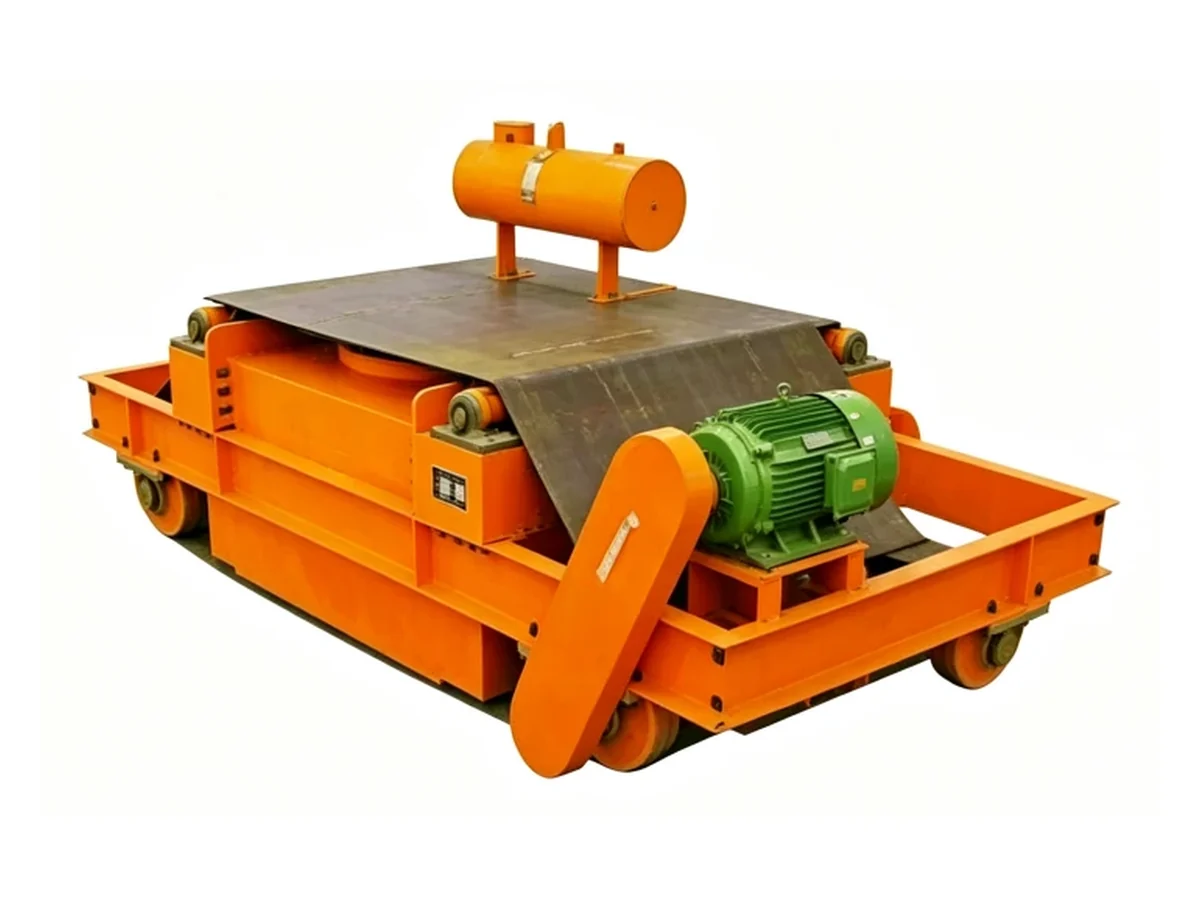
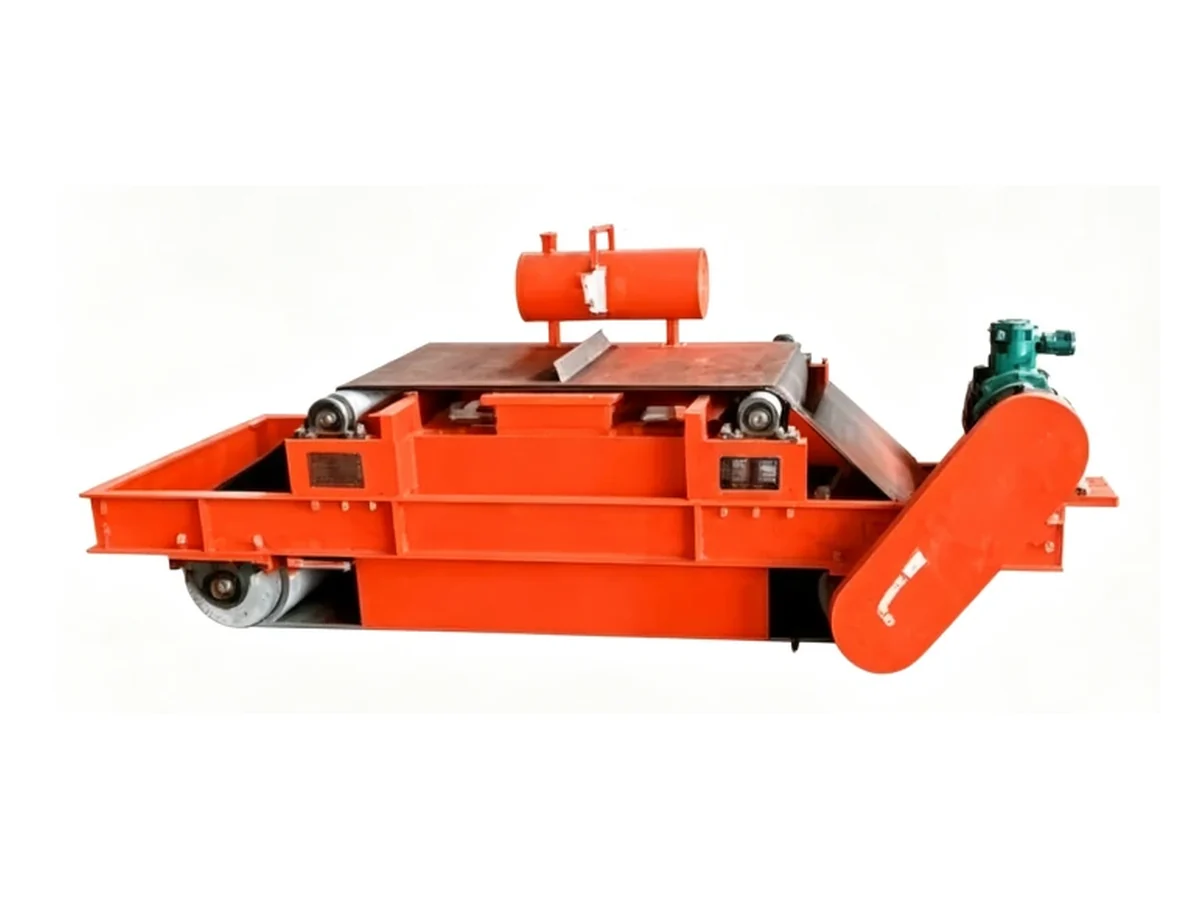
The product photos show the suspended body, cleaning belt, rollers, drive-side parts and suspension frame. Use the approved GA drawing for project dimensions and connection points. If the order includes a magnetic measurement or capture test, the test record should show the agreed condition and result.
What to Send Corvelan
Start with the material, iron you need to remove, conveyor data and installation space. For the final machine choice, also send the hardest iron piece, deepest normal material layer and working distance.
Confirm the separator type, machine setup, installation drawing, electrical requirements, cooling type, discharge direction and any test written into the order.
Check the finished separator against the order and approved drawing. Check the cleaning-belt direction and running condition, visible assembly, electrical functions in scope, and any magnetic or capture test included in the order.
FAQ
Choose it for a dry conveyor that regularly carries iron or steel and needs automatic discharge. It is a strong option when the job also needs an energized suspended magnet and oil cooling fits the running duty.
Choose air-cooled when you still need an energized magnet and automatic discharge, but the site does not want an oil-filled cooling system. The selected air-cooled design must still handle the required duty and site conditions.
Use manual cleaning when iron appears only occasionally and planned safe stops are acceptable. If cleaning would stop production repeatedly, use self-unloading.
Compare a suspended permanent magnet when it can catch the required iron at the working distance without electrical power. Use an electromagnet when the required reach or operating duty needs it.
Do not choose the separator from a generic suspension height. Measure from the magnet face to the hardest iron position inside the deepest normal material layer. That is the working distance we use.
No. Gauss is magnetic flux density at one defined point. A high Gauss number does not by itself prove pull force or moving capture at the real working distance. For critical protection, define the iron piece and test the real condition.
Deep material and high belt speed make capture harder. Do not choose the final separator from a catalog table alone. Test the required iron at the agreed distance and a similar belt speed.
Do not choose the cleaning belt from magnetic pickup alone. Tell us the iron shape and mass. Then check belt protection, impact path, guards, chute and collection system too.
No. Use a non-ferrous separator, such as an eddy-current separator, for aluminum or copper. Test stainless steel by its actual grade and condition because magnetic response can vary.
Confirm the conveyor details, required iron pieces, deepest normal material layer and working distance. Also confirm the magnet and cooling type, discharge layout, support, maintenance space, electrical requirements and test method.
Use a capture test for deep material, high belt speed, small critical iron, heavy iron or crusher protection. Use it whenever actual capture matters more than a static magnetic reading.
Do not make the test easier just to get a pass. Reduce the working distance or material depth, move the separator, use a stronger magnetic setup or choose another separator type. Then test the new agreed condition again.
For difficult applications, define the iron piece, target position, working distance and movement condition before the test. Then use those same conditions during the capture test.
The project package can include the approved drawing and the checks written into the order. If the order includes a magnetic measurement or capture test, the corresponding test record should show the agreed condition and result.
Next Step
Send the material, belt width, belt speed, normal and maximum material depth, smallest, typical and largest iron pieces, headroom and a side-view drawing or photo. We will use these details to choose the separator type, define the machine setup and agree how it will be checked for quotation.