
New bulk-material conveyor
Confirm before selection Belt width, normal and maximum material depth, target metal, installation space, and what the line should do after detection.
Find equipment by installation point and separation task.
All magnetic separators →Start with the material or production line you need to protect.
All applications →Compare technologies, check parameters and prepare your RFQ.
All guides →See the factory, quality checks and answers before you request a quotation.
Find a starting detector layout for your conveyor and detection target. Compare LJT models for bulk-material belts, existing conveyor retrofits, underbelt installations and individual product inspection. Final selection depends on the target metal, material or product dimensions, belt construction and the response required after detection.
| Your application | Starting point | Confirm before selection |
|---|---|---|
| New bulk-material conveyor | Compare LJT-A and LJT-E | Belt width, normal and maximum material depth, target metal, installation space, and what the line should do after detection. |
| Existing conveyor retrofit | Review LJT-B | Belt construction, splice or fasteners, surrounding steelwork, and access for mounting the detector. |
| Limited space around the conveyor | Review LJT-H | Available clearance, target position, and the distance from the underbelt sensor to the target. |
| Individual packaged or unpackaged products | Review LJT-F | Largest product width and height, packaging, line speed, and whether the line needs to alarm, stop, or reject. |
Confirm before selection Belt width, normal and maximum material depth, target metal, installation space, and what the line should do after detection.
Review LJT-B
Confirm before selection Belt construction, splice or fasteners, surrounding steelwork, and access for mounting the detector.
Review LJT-H
Confirm before selection Available clearance, target position, and the distance from the underbelt sensor to the target.
Review LJT-F
Confirm before selection Largest product width and height, packaging, line speed, and whether the line needs to alarm, stop, or reject.
These are starting points for comparison. Send the actual conveyor, belt and detection-target details before choosing the final model.
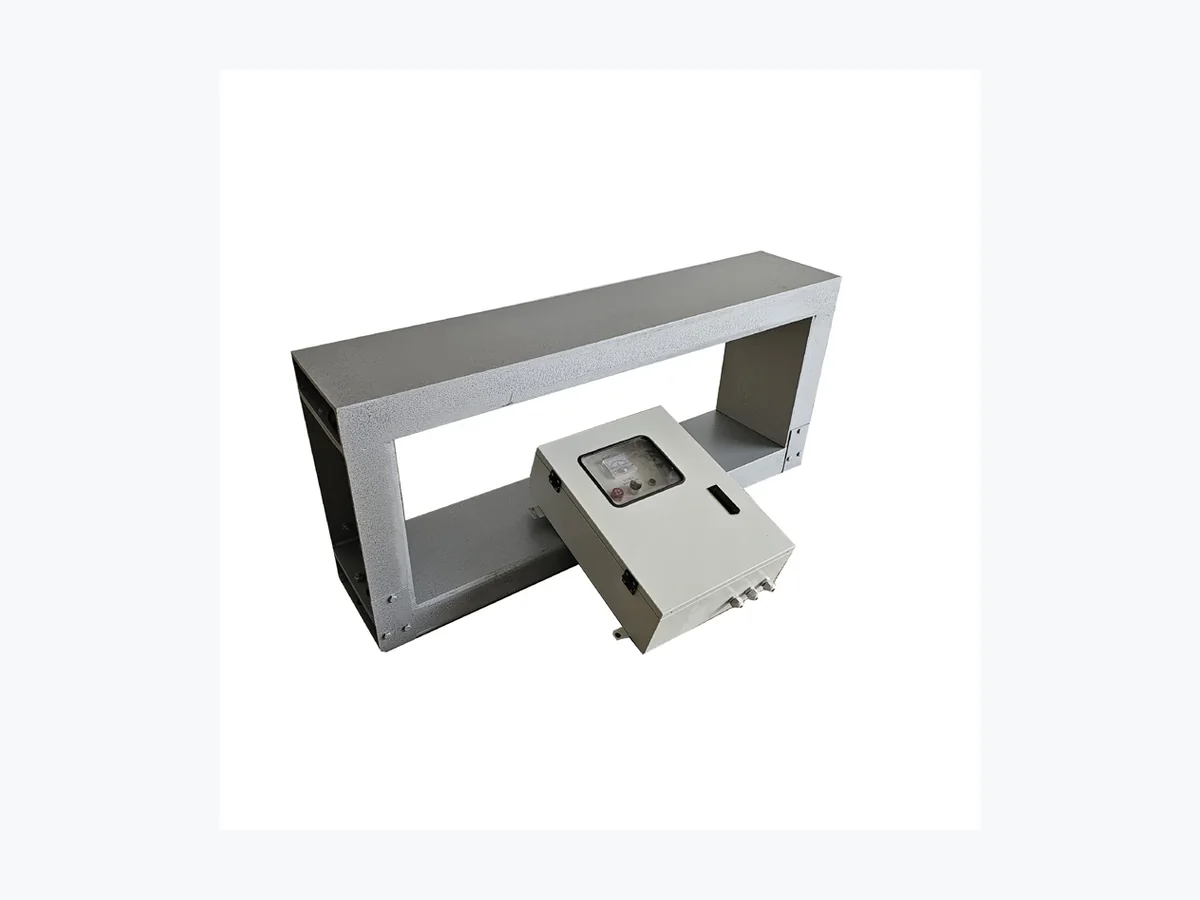
Open a model to review its layout and fit for your conveyor.
Frame-style tramp-metal detection on bulk-material belts carrying ore, coal, aggregate, or similar material.
Check first: Frame clearance and maximum material depth. Listed frame sizes cover 500–2,000 mm belt widths.
View LJT-A Details
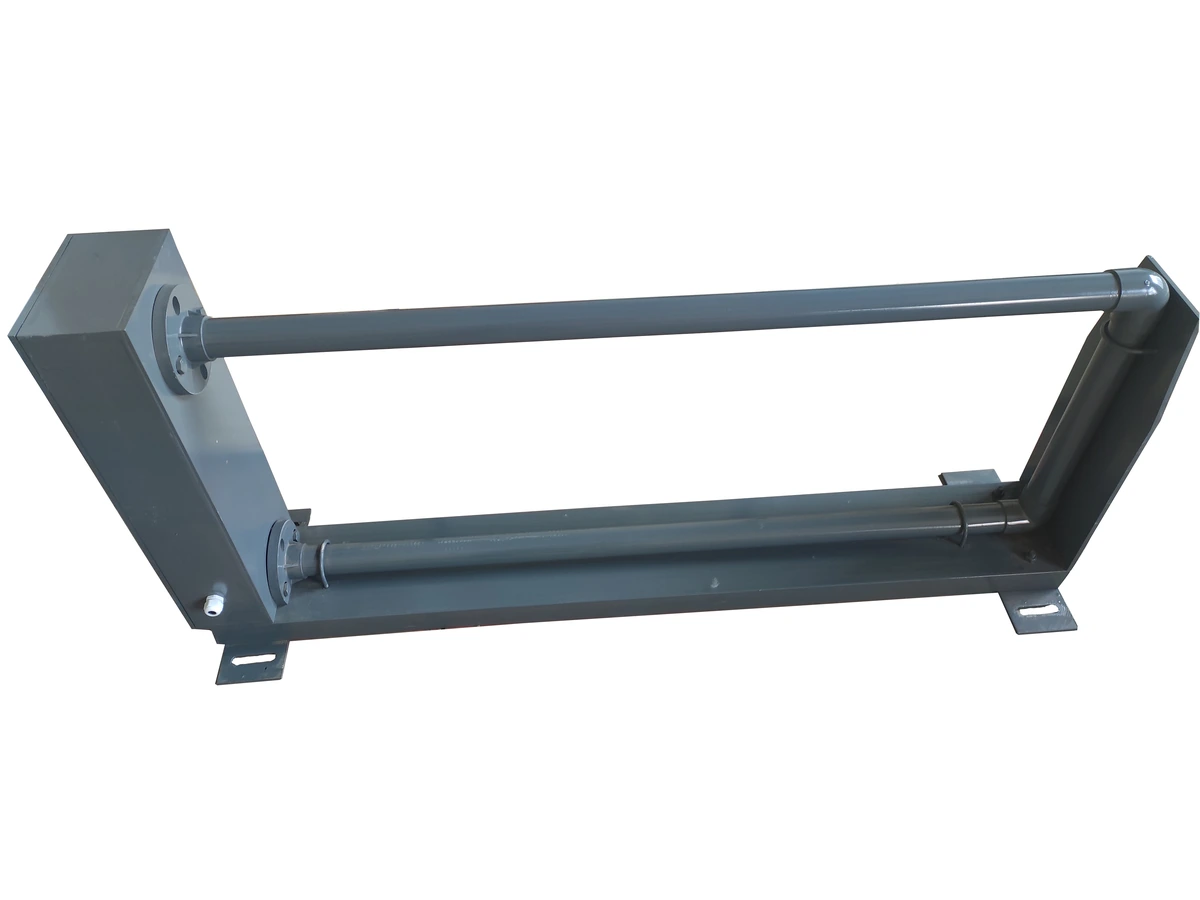
Split-frame detector designed to fit around an existing bulk conveyor without cutting the belt.
Check first: Mounting access, belt construction, and any metal splice, clips, or fasteners.
View LJT-B Details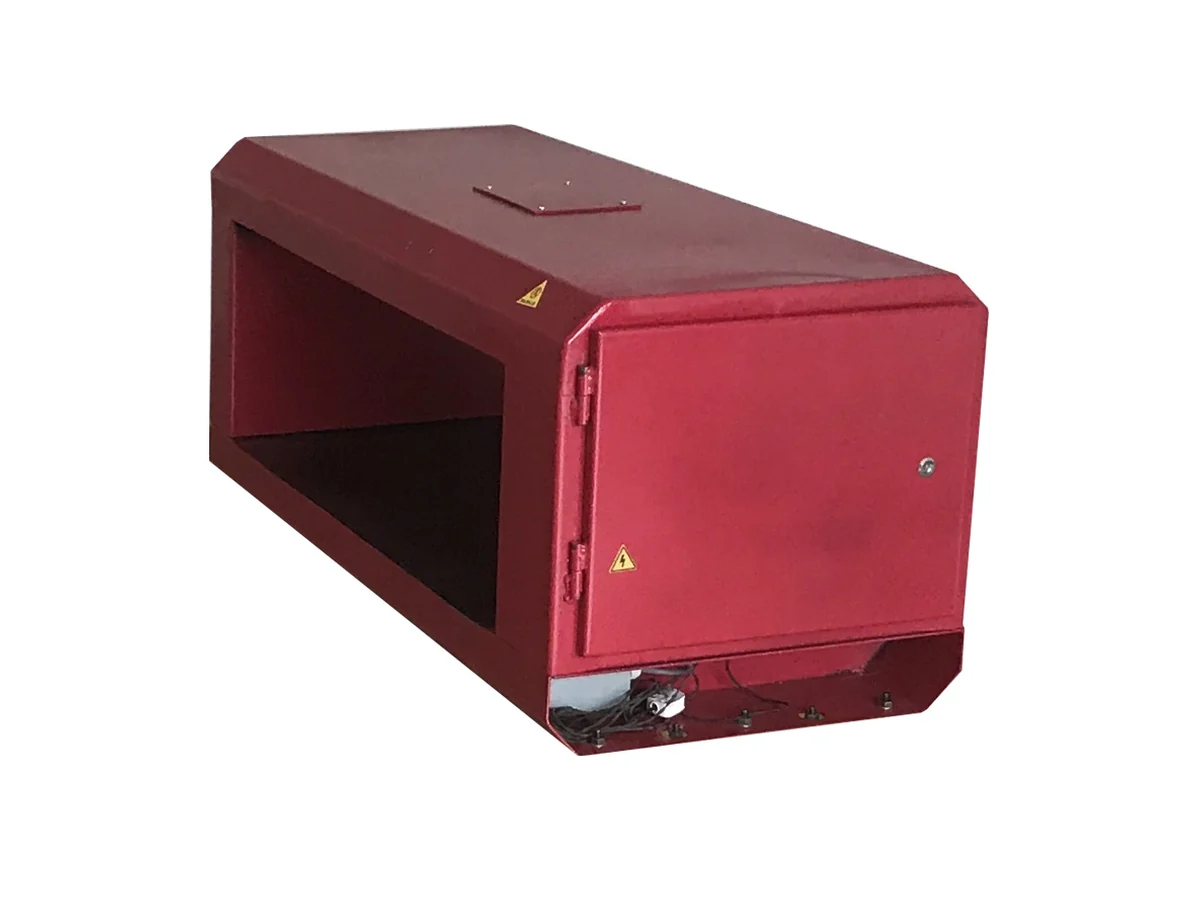
Tramp-metal detection on bulk-material belts, including applications with manganese-steel targets.
Check first: Target metal, material depth, and mounting room. Listed options cover 500–1,800 mm belt widths.
View LJT-E Details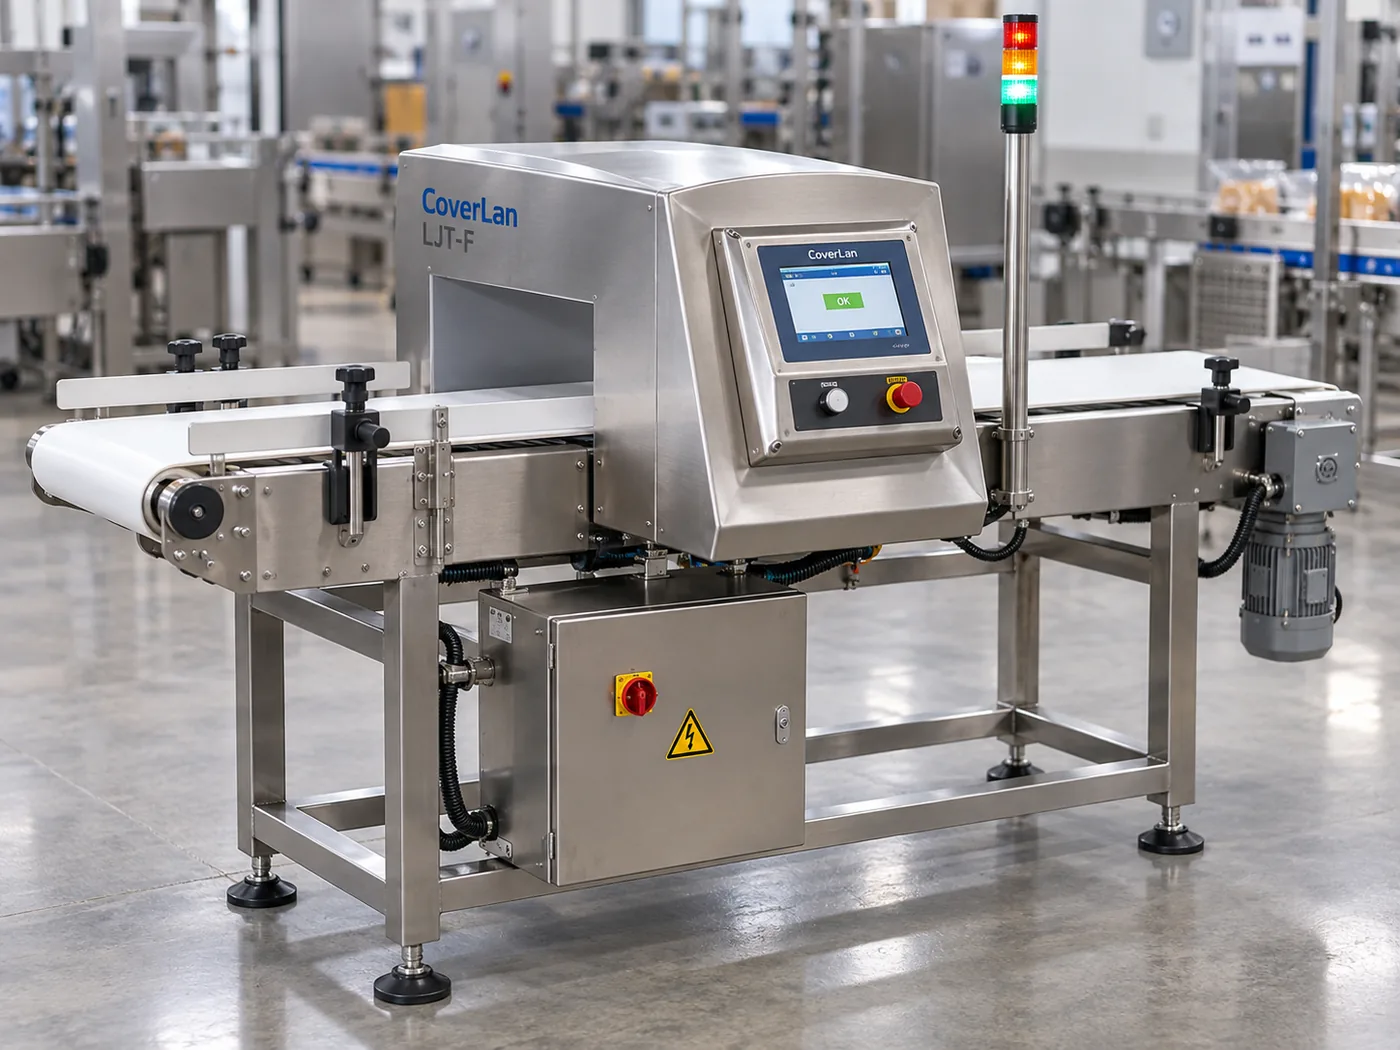
Inline inspection for individual packaged or unpackaged products passing through a detector opening.
Check first: Largest product width and height, the actual packaging, and the required line response.
View LJT-F Details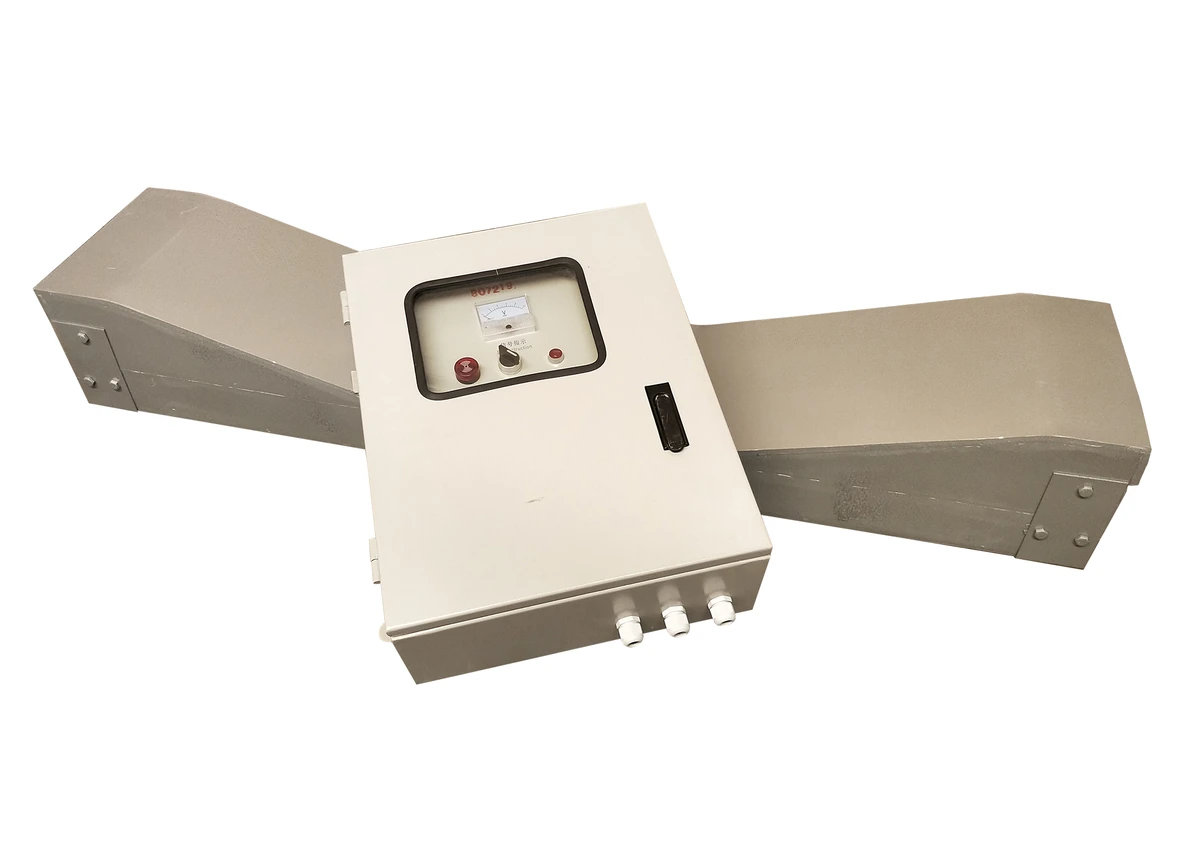
A starting option to review where space around the conveyor is limited.
Check first: Target metal, material depth, and sensor-to-target distance. Listed LJT-H-2 options cover 500–1,600 mm belt widths.
View LJT-H DetailsA deeper load, a new belt, or a different package can change what the detector sees. Use these scenarios to decide whether to keep your setup or compare another one.
On a bulk conveyor with tight clearance, an underbelt LJT-H can stay on your shortlist if it detects the required metal target through the normal shallow load. If higher throughput increases the maximum material depth, repeat the test at the new depth. If the same target is missed at the proposed sensor position, compare the frame-style LJT-A and LJT-E where there is room for a frame.
Before you order, ask the supplier to use the same metal type, size, and shape at the hardest expected target position. Test at maximum normal material depth and operating speed. Confirm that detection triggers the specified alarm or stop before the affected material reaches the crusher.
A split-frame LJT-B is a starting point when the existing belt must stay in place and the frame fits around it. If a planned replacement belt adds steel cords or a metal splice, check the signal again before keeping the original setup. If the splice repeatedly triggers alarms or the target is missed under load, ask the supplier to review the belt, mounting position, and available setup options before quoting.
Before you order, send the belt specification, splice photos, and a drawing of the proposed mounting point. Ask the supplier to check several normal splice passes for unwanted alarms and run separate loaded passes with the actual target. Confirm that the setup can distinguish the two.
If the LJT-F setup met your target with the original package, keep it in consideration when you switch to foil or metallized film. Test the new finished package first. If it fails to meet the same detection requirement, ask the supplier to review the detector opening and inspection point before specifying the new setup.
Before you order, provide finished packs, the largest pack dimensions, and the smallest metal target you must detect. Ask the supplier to test representative target positions inside the finished pack at normal speed and spacing. If automatic rejection is required, confirm that the affected pack is removed from the line.
Send your conveyor and detection details for a review of the proposed setup.
Tell us the metal type and size if you know them. “Detect metal” is usually too broad for a useful model recommendation because different metals and different target sizes do not produce the same detection result.
If iron or steel tramp metal is the main problem, first decide whether you need to detect it, remove it continuously, or do both. A metal detector gives a detection signal. A magnetic separator is used when continuous ferrous removal is the main job.
Use a metal detector when these metals must also be found. Do not rely on a conventional ferrous magnetic separator for this job. Send us the actual metal type and the smallest size that matters.
Stainless steel can be a harder target than the same size of ordinary steel in some applications. Tell us the stainless type if known, the target size, and what material or product surrounds it.
If you do not know exactly what metal may enter the line, tell us what has been found before and what damage or quality problem you are trying to prevent. Photos or real contaminant samples can help define a more useful target.
A conveyor metal detector creates a sensing field around or below the conveyor path. When a metal object changes that field enough, the controller sends a signal to the line. The line can then alarm, stop, mark, or reject, depending on how your system is set up.
These conditions can make a small metal target easier or harder to find. Check them before you choose a detector from a catalog value alone.
Smaller metal is harder to find than larger metal. The type of metal and its position can also change the signal. Tell us the smallest or most damaging target that matters.
On a bulk conveyor, a deeper material layer can place the target farther from the detector. For product inspection, an opening larger than needed can also make small metal harder to find.
Moisture, mineral content, and conductivity can change the background signal. If you inspect a wet product and need to detect a very small metal target, test the wettest normal product condition.
Steel cords, clips, fasteners, metal splices, foil, and metallized packaging can affect detection. Tell us about them before you choose the final model.
The line needs enough time and distance to stop, mark, or reject after metal is found. Product spacing also matters when individual items must be rejected.
Moving metal, steelwork, motors, power cables, vibration, and nearby magnetic equipment can make detection less stable. Choose a detector position where these effects can be controlled.
Choose the line action at the same time as the detector. Finding metal is only useful when the line does what you need next.
Use an alarm when an operator can check the event and remove the affected material or product manually.
Use a stop signal when the conveyor can stop safely and there is enough distance to find and remove the metal before it reaches the protected machine or product stream.
Use marking or automatic rejection when a product or defined section of material must be separated after detection. The timing must match line speed and the distance to the reject point.
Send us the conveyor speed, what is moving, and what you want to happen when metal is found. We can help match the detector and line action.
Help Me Choose a Detector| What you need | Choose | Why |
|---|---|---|
| Know that unwanted metal entered the line and trigger an alarm, stop, or control signal | Conveyor metal detector | You need to detect a metal event and make the line respond. |
| Continuously remove suitable magnetically responsive ferrous metal | Magnetic separator / conveyor magnet | Your main job is physical ferrous removal. |
| Detect a wider range of metal and also remove ferrous metal continuously | Use both | The detector and magnetic separator do different jobs and can be used together. |
Install the detector before the machine or product point you want to protect. Keep it away from avoidable moving metal and leave enough distance for the conveyor to stop or reject after detection.
| What to check | Why it matters | What to send us |
|---|---|---|
| Conveyor shape | The detector must fit your flat or troughed conveyor and stay close enough to the material for reliable detection. | Belt width, conveyor cross-section, flat/troughed shape, and available space. |
| Material depth | A deeper material layer, often called burden depth, can place the metal farther from the detector. | Material type, normal and maximum depth, particle or lump size, and moisture when relevant. |
| Belt construction | Steel cords, clips, fasteners, and metal splices can affect detection. | Belt specification and clear photos of the splice or fasteners. |
| Nearby metal | Moving steel and nearby metalwork can disturb the detector. | Side and top photos showing rollers, steelwork, and moving parts. |
| Motors and electrical equipment | Motors, power cables, motor drives, and nearby magnetic equipment can affect a sensitive detection area. | A simple equipment layout or marked installation photos. |
| Distance after detection | The line needs enough distance to stop, mark, or reject at the real conveyor speed. | Line speed, distance from detector to stop/reject point, and required action. |
A side photo, top photo, and simple conveyor sketch give us a starting point for reviewing the detector location. Read the conveyor metal detector installation and line response guide.
Compare where the target passed in the original test with where it can sit in a loaded belt. Recheck under normal and maximum material depth using the same target.
Check material depth and sensitivityCheck whether the alarm repeats at the splice or follows a change in mounting, nearby moving metal, or operating conditions.
Review conveyor installation conditionsCheck the configured line action, then verify timing and available stopping or rejection distance at the operating speed.
Review stop and reject setupThe detector may fit the belt but still place small metal too far from the strongest sensing area. Material depth matters as well as belt width.
Steel cords, clips, fasteners, or metal splices can create problems if they are not known before ordering.
The detector can find metal but still fail to protect the process if the conveyor cannot stop or reject in time.
A sensitivity value measured with a different product, material depth, detector opening, or installation may not match your real conveyor.
For product inspection, use the smallest practical opening that safely passes the product. A larger opening can make small metal harder to detect.
If the real job is continuous ferrous removal, a detector alone is not the right starting point.
If the smallest detectable metal size matters to your order, tell us the target clearly. This is much more useful than asking for “high sensitivity.”
Tell us whether the target is iron/steel, stainless steel, non-ferrous metal, or another known metal. Add the size and shape if you know them.
For bulk material, tell us the normal and maximum material depth. For product inspection, tell us the largest product size and where the metal may sit inside the product.
Tell us the line speed and the normal product, packaging, or material condition. If one normal condition is harder to inspect, send that condition too.
A conveyor metal detector checks bulk material or individual products while they move on a conveyor. When metal creates a strong enough signal, the detector can send an output for an alarm, stop, mark, reject, or other line action.
For a new bulk conveyor, compare LJT-A and LJT-E first. Choose LJT-B first for an existing conveyor where you do not want to cut the belt. Check LJT-H when installation space is tight and an underbelt sensor can stay close enough to the target. Choose LJT-F for packaged or unpackaged products that pass through a detector opening.
Yes, conveyor metal detectors can be used for non-ferrous targets as well as ferrous metal. The metal type, size, product or material, and installation all affect the result, so send us the actual target you need to find.
Stainless steel can be part of the detection target, but the result depends on the stainless type and size as well as the product or material around it. Tell us the stainless target you need to find instead of asking only for “metal detection.”
The detector finds the metal and sends a signal. Removal needs another action, such as stopping the belt for manual removal, rejecting an individual product, or using a magnetic separator for suitable ferrous metal.
No. For product inspection, use the smallest practical opening that safely passes your largest normal product. An opening larger than needed can make small metal harder to detect.
Do not choose the detector from belt width alone. Steel cords, metal clips, fasteners, and splices can affect detection, so send us the actual belt construction before choosing the final model.
Install it before the machine or product point you need to protect. Keep the detection area away from avoidable moving metal and leave enough distance for the conveyor to stop or reject after metal is found.
Metal type and size, material depth, detector opening, product or material condition, belt construction, packaging, speed, nearby metal, vibration, and electrical equipment can all affect how small a target can be found.
Choose a metal detector when you need to know that metal entered the line and want an alarm, stop, or reject signal. Choose magnetic separation when the main job is continuous removal of suitable ferrous metal. Use both when you need both functions.
Send us what is moving, the metal you need to find, the belt or product dimensions, and what you want the line to do after detection. Conveyor photos and belt or packaging details are also helpful.
No. Belt width helps with physical fit, but you should also check material or product size, target metal, belt construction, installation space, line speed, and the action needed after detection.
The loaded material can change the background signal, increase the distance between the target and detector, or change how the target passes through the sensing area. Check the real material depth and product condition, not only the empty-belt result.
Check for metal in the belt, loose or moving steelwork, changed splices or fasteners, nearby motors or cables, vibration, and changes in the material or product. Find what changed before changing detector settings at random.
Send us the normal and maximum material depth. If small metal matters, the deeper condition is usually the more important one to check because the target can be farther from the detector.
Send the details you already have. Conveyor photos and a clear description of the metal target can help us identify the starting layout and any information still needed for selection.
If available, include conveyor photos, belt or splice details, and packaging information.
Open the Contact Form