
Best Fit
Dry conveyor-fed bulk material, responsive iron or steel tramp, enough headroom and support, and a planned cleaning stop that fits the process.
Find equipment by installation point and separation task.
All magnetic separators →Start with the material or production line you need to protect.
All applications →Compare technologies, check parameters and prepare your RFQ.
All guides →See the factory, quality checks and answers before you request a quotation.
Corvelan supplies air-cooled suspended electromagnetic separators for removing unwanted iron and steel from conveyor-fed material before it reaches crushers, mills, screens and other downstream equipment. We size the separator from your belt width, material depth, real working distance, target tramp iron and site conditions, then confirm the project-specific details on the quotation and approved drawing.
The air-cooled design uses forced air to manage heat without an oil-filled cooling circuit. If captured tramp iron must discharge automatically, Corvelan can select a self-cleaning cross-belt electromagnetic separator instead.
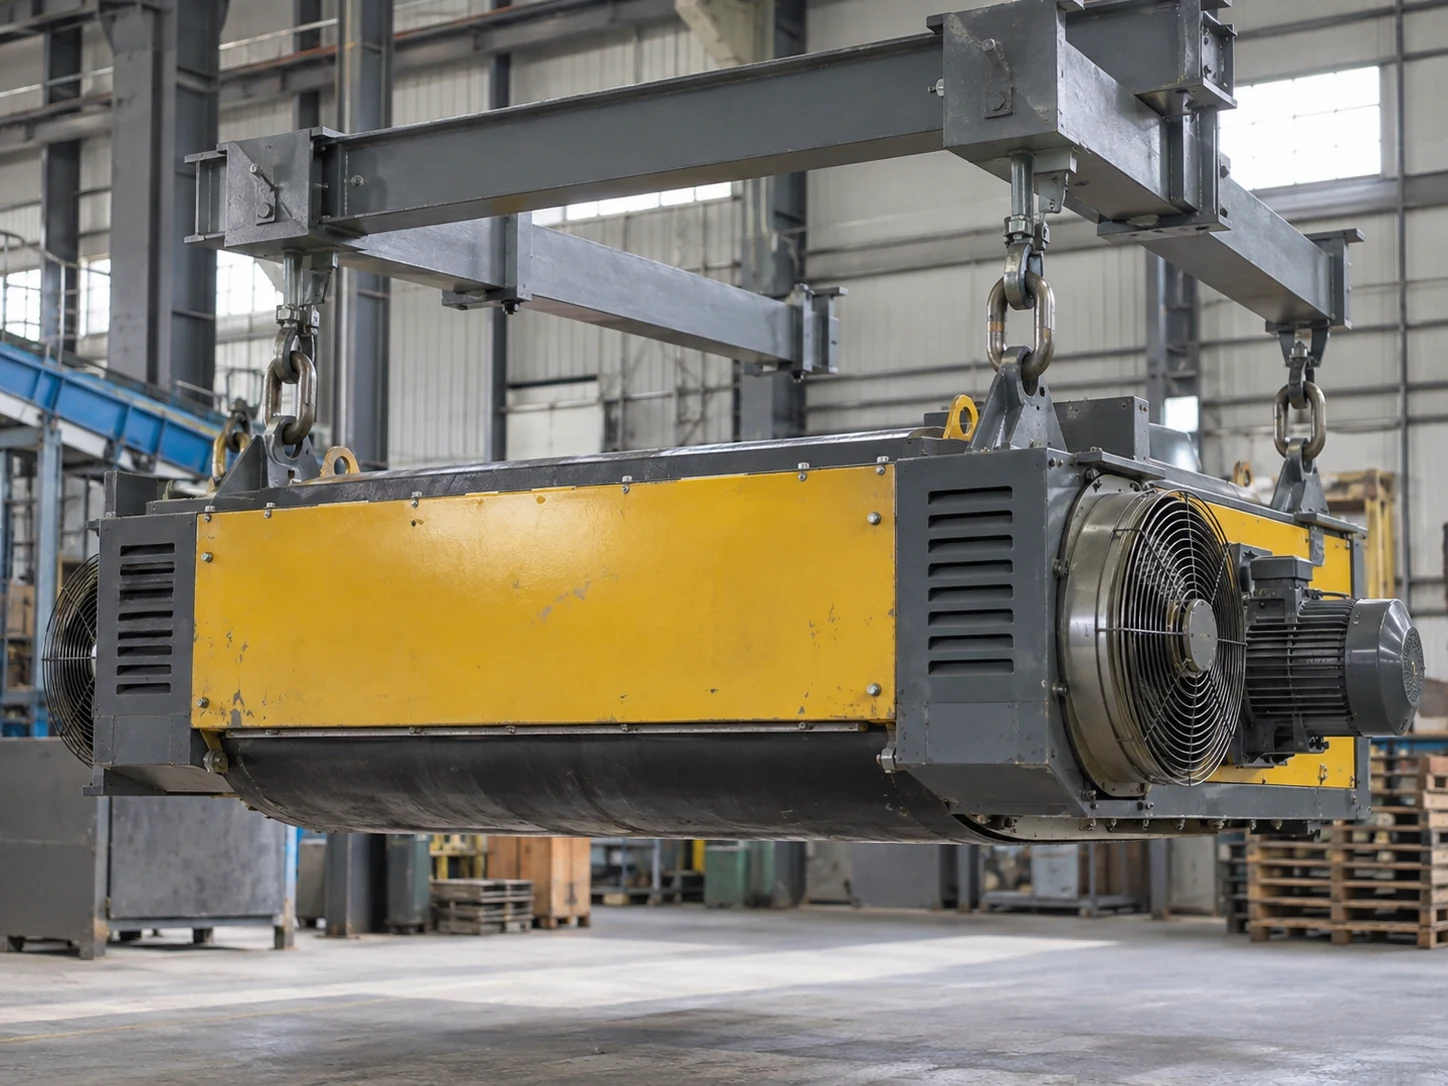
This separator works well when the main target is iron or steel that responds strongly to a magnet. There must also be enough room above the conveyor, and planned cleaning must be practical. We check the conveyor before selection because material depth, working distance, belt speed and site conditions can change the separator size and setup.
Dry conveyor-fed bulk material, responsive iron or steel tramp, enough headroom and support, and a planned cleaning stop that fits the process.
Deep or uneven material, high belt speed, large or buried tramp pieces, restricted headroom, heavy dust, unusual ambient temperature or limited airflow.
Choose a self-cleaning separator when tramp iron must discharge automatically. Use a magnetic head pulley when separation is best at the conveyor discharge point, or a magnetic drum when the process needs controlled split-stream separation. Non-ferrous metals require another separation technology.
Corvelan uses this equipment for conveyor-fed bulk material where the target is iron or steel that responds strongly to a magnet. This is often called ferromagnetic tramp iron. For selection, we need to know the hardest piece to remove and how deep it can sit in the material. We also check whether the surrounding material can trap it in place.
Mineral, aggregate, coal, recycled material, biomass or other conveyor-fed solids may be reviewed, provided the actual flow and site conditions are defined.
Bolts, steel fragments, tools, wire and other magnetic iron or steel pieces can be targets. For critical tramp iron, tell us the size, shape, weight, likely position and how often it appears.
Aluminum, copper and other non-ferrous metals need another separation technology. Fine or weakly magnetic mineral particles usually need a high-intensity separator and application testing.
Corvelan uses an energized electromagnet suspended above the conveyor to create the working magnetic field. As material passes below, iron and steel pieces can be pulled upward when the magnetic force is strong enough at their actual position in the material. Captured iron stays on the magnet face until planned cleaning. If automatic discharge is needed, we use a self-cleaning cross-belt electromagnetic separator.
Belt speed and material depth on the belt, often called burden depth, affect how the target moves through the magnetic zone.
Distance and target shape matter. We also check how tightly the piece is trapped in the material and how strongly it responds to the magnetic field.
The separator must provide useful field and force at the target location, not only a high reading at the magnet surface.
Corvelan matches the cleaning method to how often tramp iron is collected. Planned cleaning works for lower or occasional tramp loading. If iron must discharge automatically and frequently, we recommend a self-cleaning cross-belt electromagnetic separator.
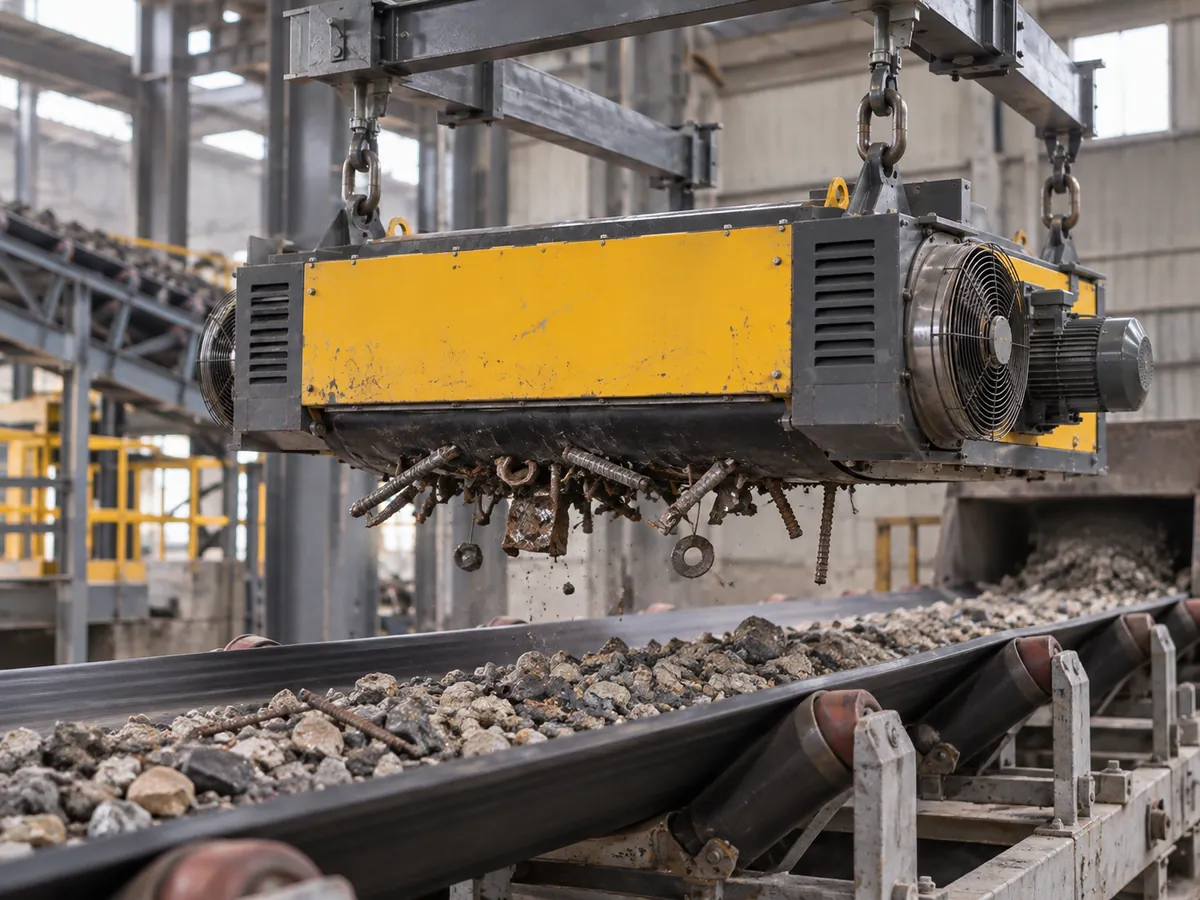
Corvelan uses an air-cooled suspended electromagnet when forced-air cooling suits the required performance and site conditions. We check how long the separator runs, ambient temperature, available airflow, dust exposure and maintenance access before confirming the cooling design.
The air-cooled design does not use an oil-filled cooling circuit. This can simplify the cooling system when forced-air cooling matches the operating conditions.
We review continuous or intermittent operation, electrical loading, ambient conditions, airflow and dust before confirming the cooling arrangement.
Voltage, excitation power, fan arrangement, enclosure and controls are confirmed for the final separator and the site requirements.
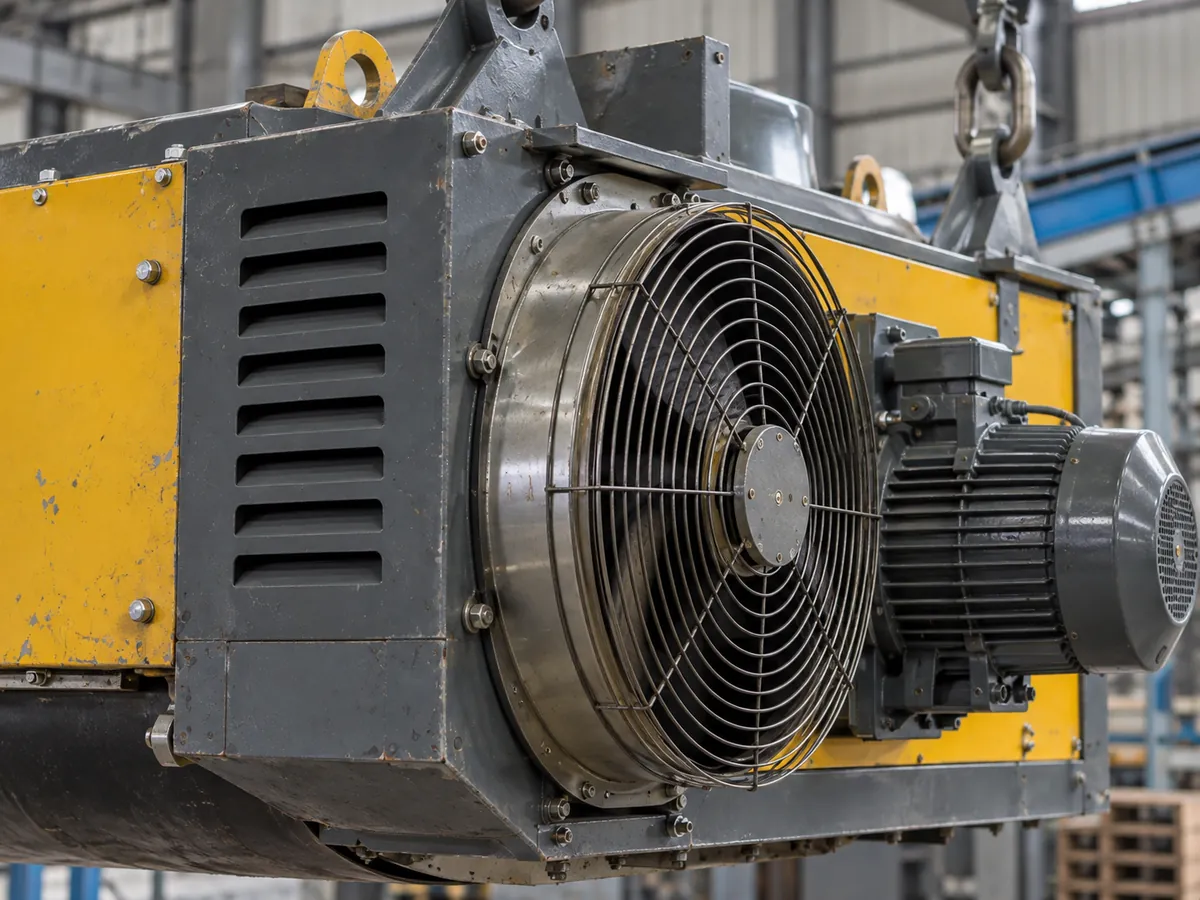
A high surface Gauss reading does not tell the whole story. We also check the distance to the iron and how deep it sits in the material. Belt speed and the type of tramp iron also matter. Corvelan sizes the separator for the real working distance, not only the reading at the magnet surface.
Iron near the belt can be much farther from the magnet than iron visible at the top of the material. We therefore check both normal and maximum material depth.
Use the distance from the magnet face to the hardest target position. Include mechanical clearance and how deep the target can sit in the material.
Size, shape, mass, orientation, magnetic response and frequency affect how easily a piece can be lifted free.
Higher speed shortens exposure time through the useful magnetic zone and can affect material trajectory.
Particle size, bulk density, moisture, lumping and feed stability can bury or trap ferrous contamination.
Trough profile, surrounding steel, support structure, headroom and cleaning access can change both magnetic and mechanical suitability.
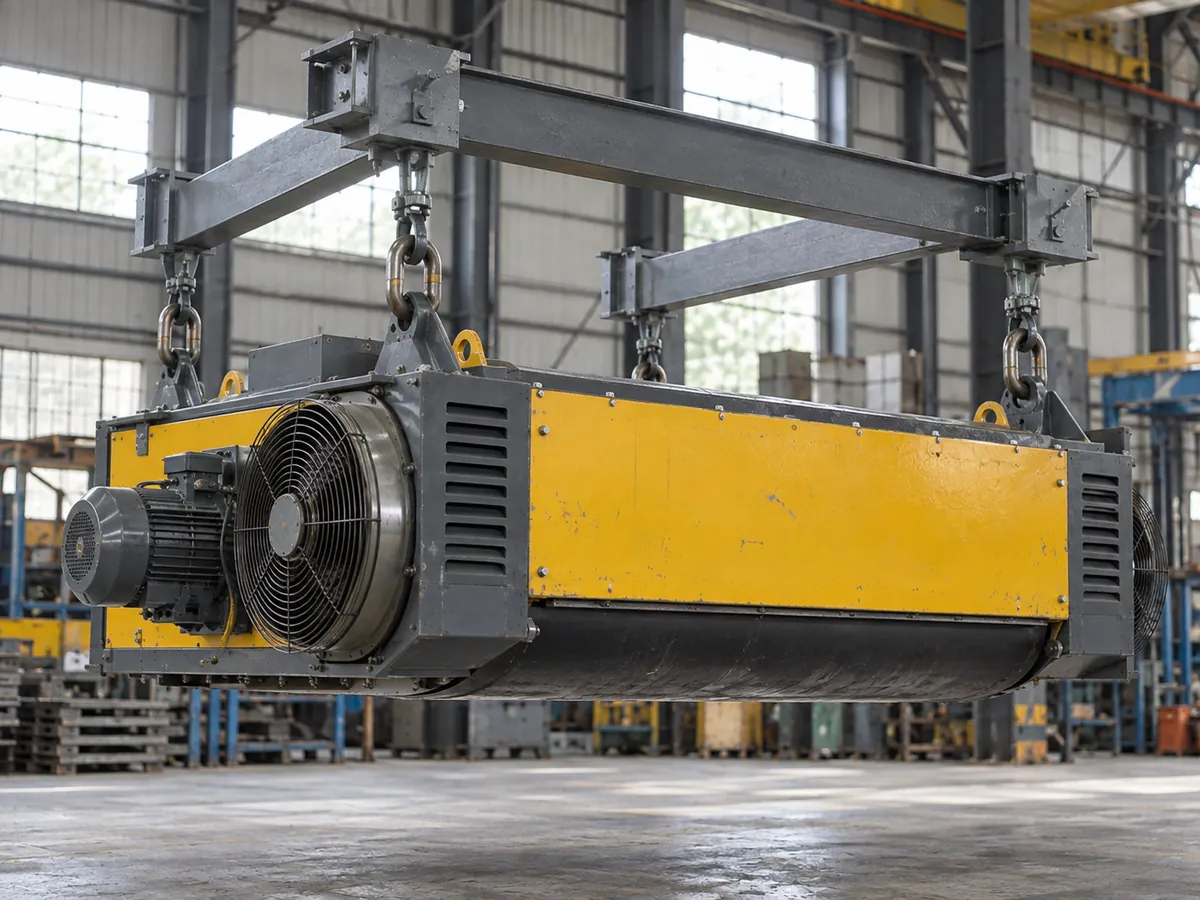
We start with your real conveyor conditions. Then we check magnetic coverage, working distance, suspension, cleaning, cooling, power and controls. This keeps the quoted separator tied to your process instead of a generic catalog assumption.
| What we check | Why we need it |
|---|---|
| Magnetic coverage | We confirm belt width, material width and the actual path the magnet must cover. |
| Real working distance | We use the distance from the magnet face to the hardest target position. This includes mechanical clearance and how deep the target sits in the material. |
| Suspension & installation | We review headroom, support points, surrounding steel, service access and the proposed separation position. |
| Cleaning method | We match planned cleaning or self-cleaning discharge to expected tramp frequency and process interruption limits. |
| Air cooling | We review running time, ambient temperature, airflow, dust exposure and maintenance access before confirming the cooling design. |
| Electrical & controls | We confirm the required power supply, rectifier and controls, isolation, start/stop connection and any project-specific alarms or interlocks. |
Corvelan chooses the separator type from the target metal, working distance, running conditions and cleaning needs. The table below shows when each type is a good fit before we choose the exact model.
| Separator type | Good choice when | What to check |
|---|---|---|
| Air-cooled suspended electromagnet | A powered suspended magnet with forced-air cooling fits the site conditions, and planned cleaning is practical. | Can the required magnetic performance be achieved at the real working distance and site temperature? |
| Oil-cooled suspended electromagnet | An oil-cooled electromagnet is preferred when oil cooling better suits the operating conditions or heat-management needs. | Which cooling method best matches running time, environment, maintenance and project requirements? |
| Suspended permanent magnet | A permanent magnet is preferred when excitation power is not wanted and the required magnetic performance can be achieved without it. | Can the permanent magnetic circuit meet the target at the required working distance? |
| Self-cleaning cross-belt electromagnet | Tramp iron is frequent or captured metal must discharge automatically without repeated manual cleaning stops. | Where will the discharge belt send the captured iron, and is there space for drive, tracking, guarding and access? |
Corvelan sizes this separator for the actual conveyor instead of using one universal specification for every installation. Our quotation and approved drawing confirm the main dimensions, power and control scope, suspension arrangement, magnetic requirements, cooling design and any agreed test or inspection requirements.
| What we need | What we confirm |
|---|---|
| Conveyor | Belt width, belt profile, speed, normal and maximum material depth, and material path. |
| Magnetic requirement | Target tramp description, required working distance and any agreed capture or test condition. |
| Electromagnet | We confirm the magnetic design and cooling arrangement. If a magnetic reading is required, we also define the measuring point. |
| Electrical | We confirm the power supply, rectifier/control panel, wiring connection, isolation and any site-specific control requirements. |
| Mechanical | Overall dimensions, suspension points, lifting and service access, clearances and nearby steelwork. |
| Environment & safety | Ambient conditions, dust or corrosion exposure, hazardous-area requirements, guarding and other site safety requirements. |
| Test and inspection | Approved drawing revision, inspection points, test method, measuring instrument and position where needed, and the result that must be met. |
Different documents prove different things. Corvelan ties each important project requirement to the right drawing, inspection item or test instead of using one magnetic number to stand in for the whole machine.
| Evidence | What it can confirm | What it does not prove by itself |
|---|---|---|
| Approved drawing | Main dimensions, suspension points, clearances, connection positions and the agreed installation layout. | It does not prove tramp-iron capture or separation efficiency. |
| Magnetic measurement record | Magnetic flux density at a defined point, distance, direction and test condition. | A Gauss reading at one point does not prove capture on a moving conveyor. |
| Electrical or functional check | Energization, cooling fan operation and the control functions included in the agreed project scope. | It does not prove separation efficiency. |
| Representative tramp test | Capture performance for the agreed test piece, material condition, material depth, belt speed and working distance. | The result should not be treated as universal outside the recorded test conditions. |
| Photo or inspection record | Physical construction, assembly condition and the items visible at the recorded inspection point. | A photo is not a substitute for measured magnetic or separation performance. |
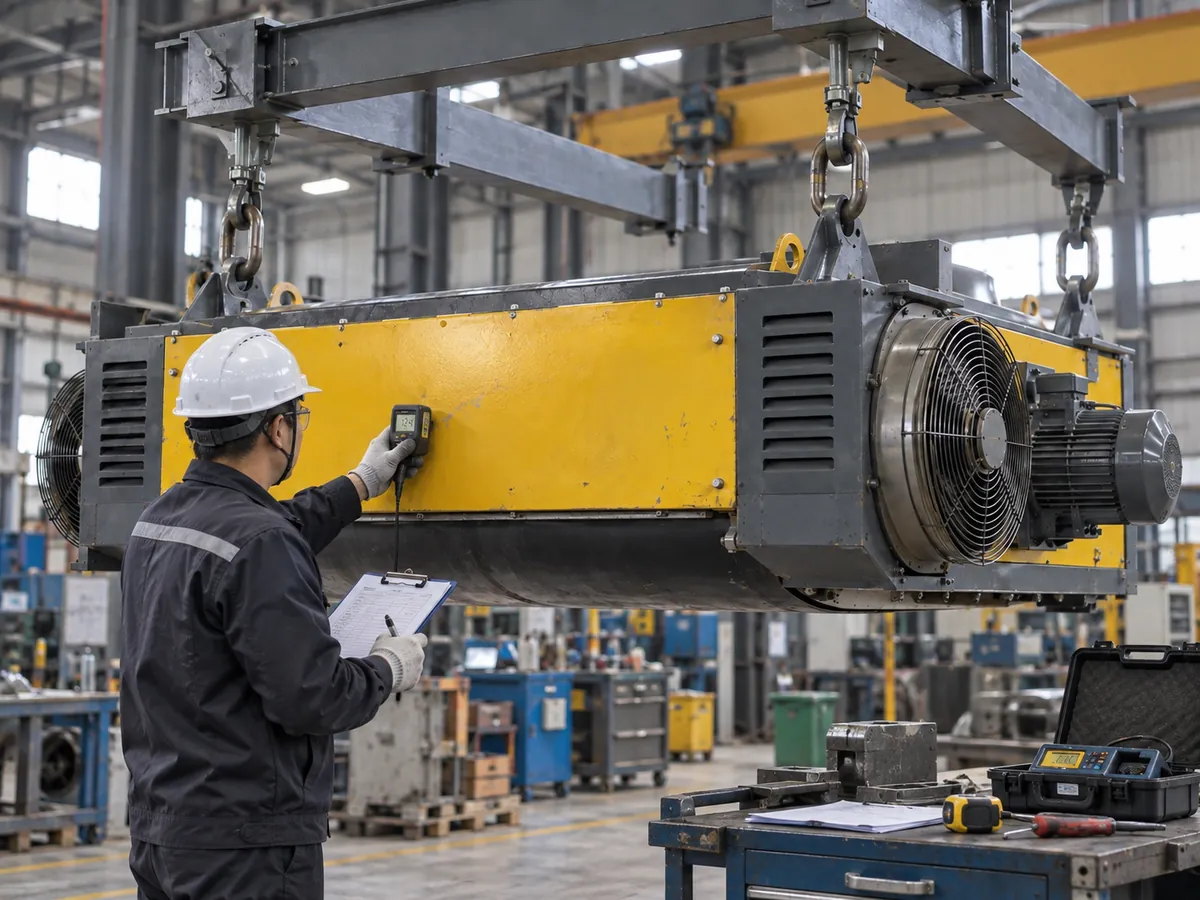
We recommend this equipment when removing tramp iron from a conveyor is the main job and the installation, cleaning and air-cooling conditions fit the application. If another separator type suits the target, cleaning need or installation point better, Corvelan will change the selection before quotation.
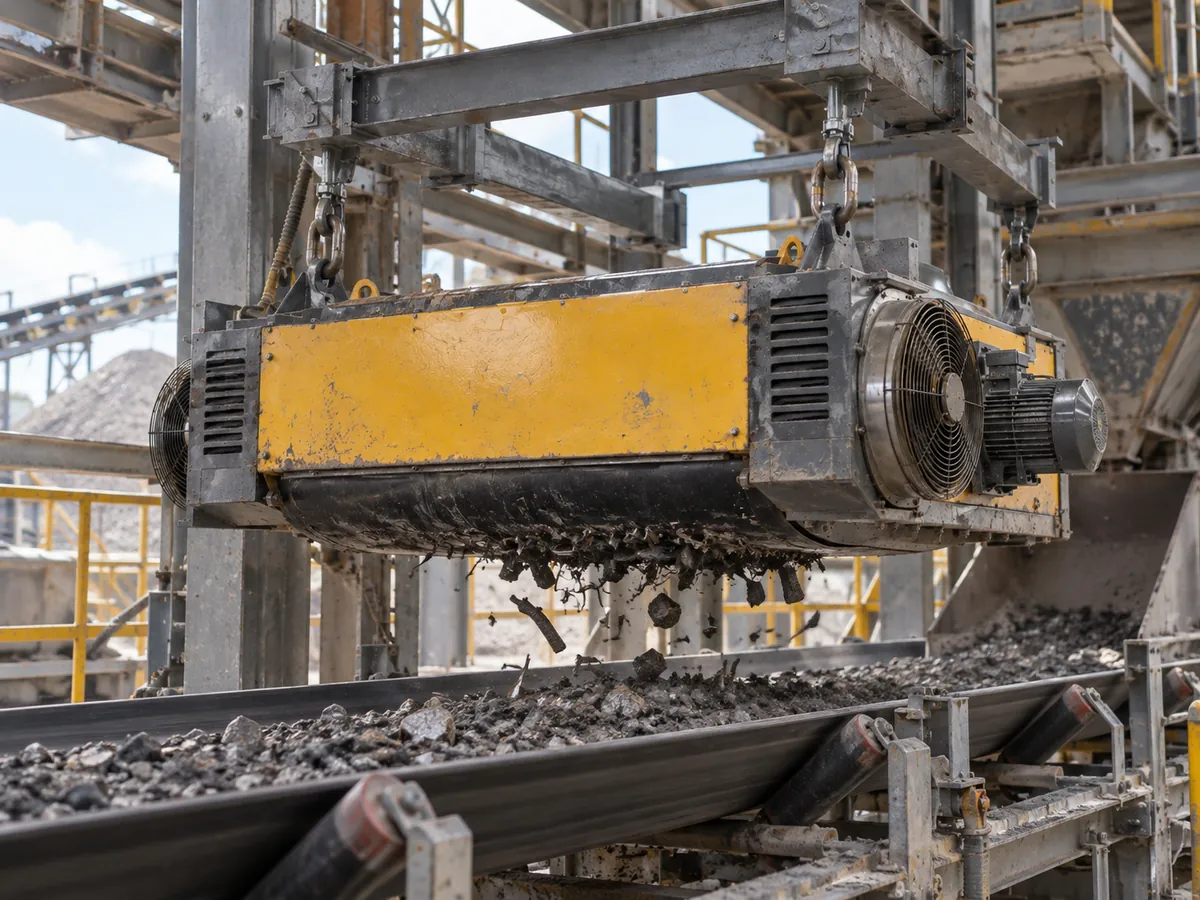
Corvelan checks the conveyor layout, magnetic working distance and service access before finalizing the installation. A photo or drawing lets us check the real working gap, support structure, nearby steel, cable and control path, and the space needed for maintenance.
Confirm structural support, suspension points, lifting path and adjustment method for the selected equipment mass and geometry.
Show the belt profile, material depth, deepest target position and nearby ferrous steel that could interact with the working field.
Provide a safe path for removing captured metal and enough space for tools, collection and maintenance after the equipment is isolated.
Confirm where power and controls will connect and how cables will run. We also confirm how the separator will be isolated and what Corvelan supplies versus what connects to the plant control system.
Place the separator early enough to remove target tramp before the equipment that needs protection, while still maintaining a workable magnetic path.
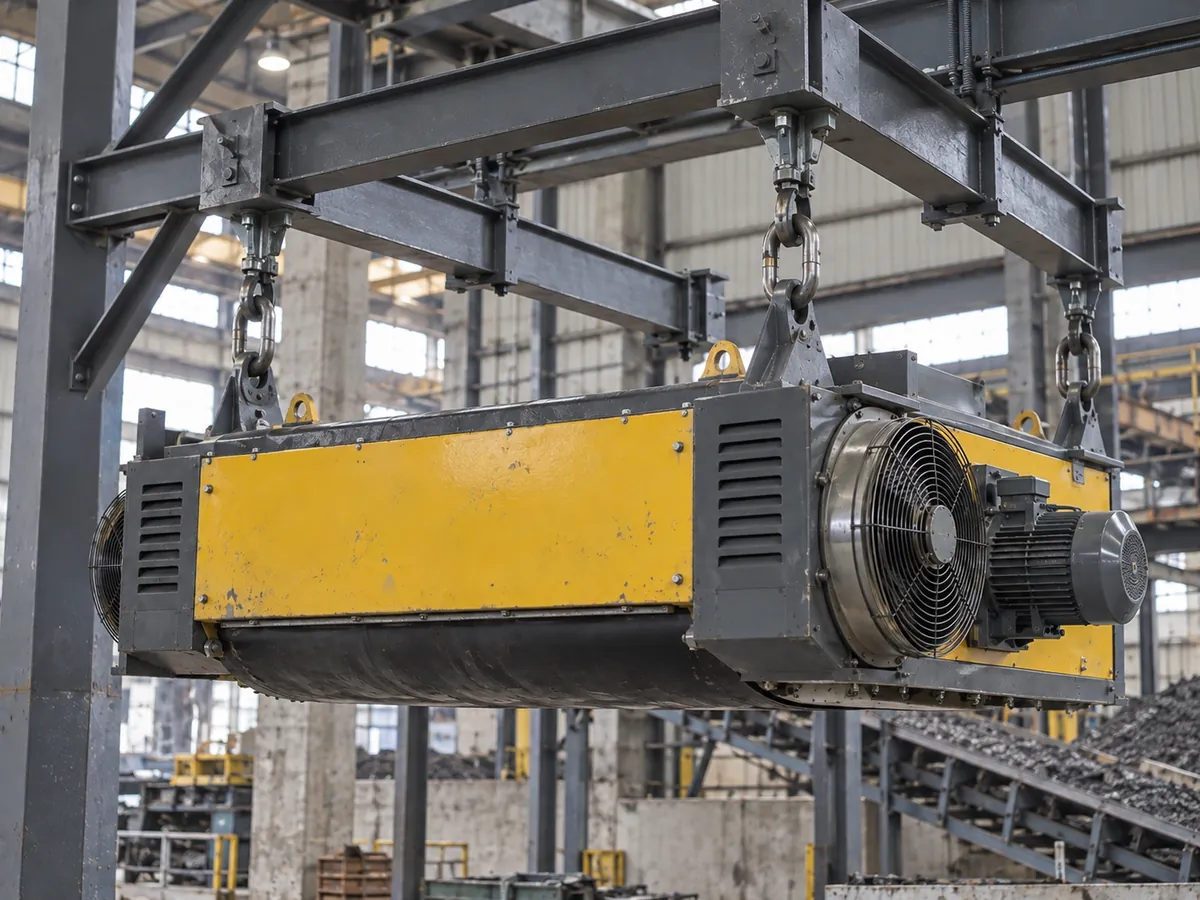
We plan cleaning and maintenance around the expected tramp loading, service access and site safety procedure. The final arrangement must account for the active magnetic field, electrical equipment, suspended mass and the maintenance access zone.
Stop and isolate the relevant equipment according to the site procedure before cleaning or maintenance. Confirm the final lockout sequence from the selected electrical and mechanical scope.
Keep loose ferrous tools and uncontrolled steel objects away from the active field. Site rules should address magnetic hazards for personnel and sensitive devices.
Check suspension hardware, fasteners, electrical connections, cooling passages or fans where fitted, magnet face condition and any accumulation that affects cleaning.
Tell Corvelan if the project requires a specific IP, CE, ATEX, hazardous-area, washdown or other compliance condition. We confirm applicable requirements only from the quoted equipment and supporting project documents.
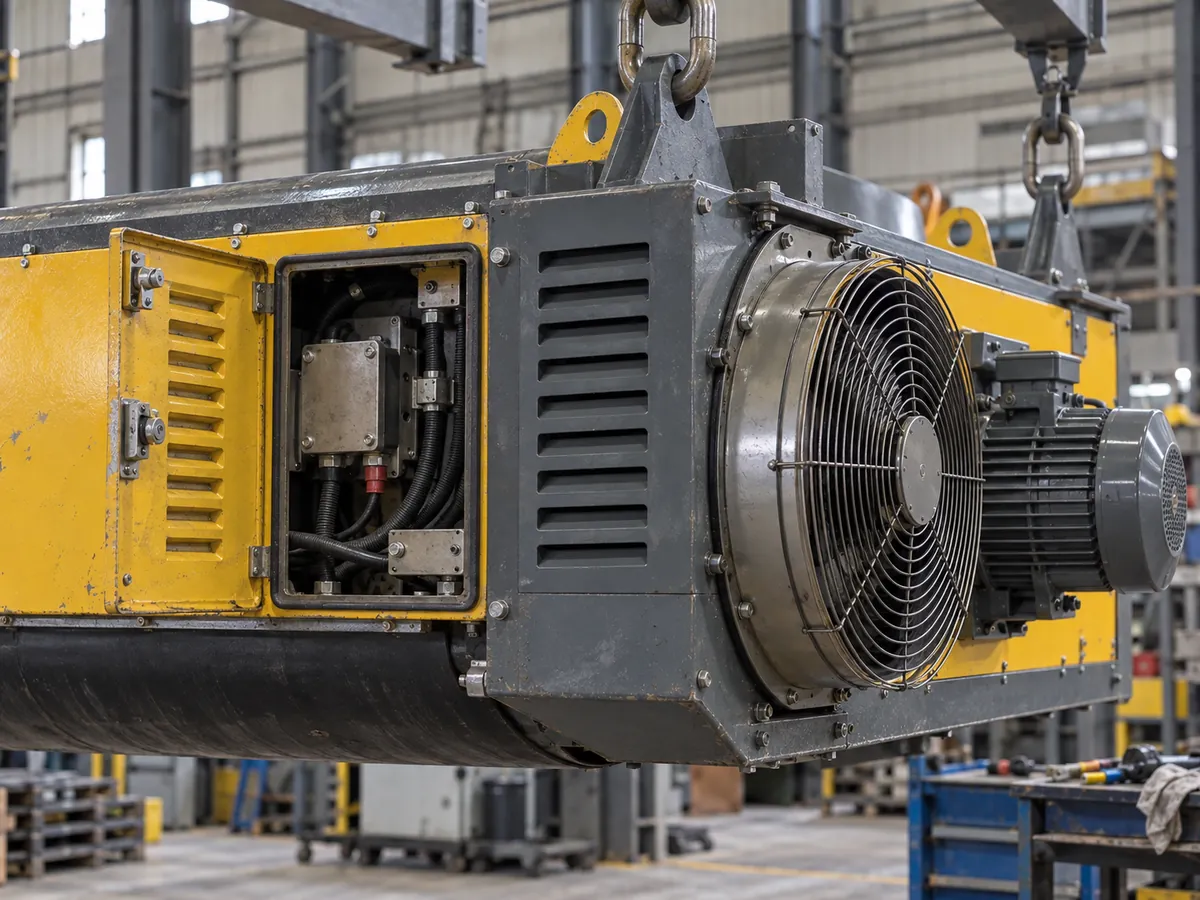
Before we promise a test result, we first agree on what will be tested and how we will check it. A magnetic field reading can confirm the field at one defined point. By itself, it does not prove capture rate, throughput or removal efficiency under real conveyor conditions. If performance testing is required, Corvelan agrees the test conditions and pass/fail requirement before order.
If magnetic flux density, often reported in Gauss, is part of the inspection, we agree the instrument, probe direction, measuring position, distance, temperature condition and required range.
If capture performance must be tested, we agree the test piece, material condition, material depth, belt speed and working distance. We also agree the number of passes and the pass/fail requirement.
Check suspension points, clearances, magnet position and approved connection points against the project drawing.
If included in the project, we check energization, controls, alarms or interlocks, and cooling function against the approved electrical specification.
If a project requires a capture result, the result only has value when the test conditions are recorded with it. We define the target piece, conveyor condition and pass/fail requirement before the test so the result can be traced back to the conditions that produced it.
Record the material, particle or lump size where relevant, feed width, material depth and any condition that could bury or trap the target iron.
Record the test piece size, shape, mass, material and where it is placed in the material.
Record belt width, belt speed, trough profile and the actual separation point used during the test.
Record the distance from the magnet face to the target position, not only the clearance above the top of the material.
Record the number of passes, separator settings and the agreed pass/fail requirement.
Record what happened under those conditions. The result should stay tied to the stated test conditions and should not be presented as a universal efficiency claim.
Corvelan turns your conveyor information into a separator choice that can be quoted, installed and checked. Before order, we define the main equipment setup, installation points, power and controls, and any drawing or test requirements that are part of the project.
We confirm the material, target tramp iron, belt width, belt speed, material depth, installation point and relevant site conditions.
We define the suspended electromagnet type, cleaning method, air-cooling design and required working distance.
We confirm suspension space, clearances, surrounding steel, lifting and service access, and the dimensions that must appear on the project drawing.
We confirm the required power supply, what is included with the rectifier and controls, and what must connect to the plant system.
When required, we agree dimensional checks, magnetic measurement points, functional checks or representative tramp testing before order.
The quotation records the agreed separator, included equipment and the project-specific items that still need drawing or test confirmation.
There is no universal installation height for every conveyor. Corvelan uses the real distance between the magnet face and the hardest target iron, including mechanical clearance and how deep the iron can sit in the material. Send the belt profile, material depth and available headroom so we can check the working distance.
Neither cooling type is automatically better. The right choice depends on running time, ambient temperature, airflow, dust exposure, maintenance needs and project requirements. Corvelan uses air cooling when it can meet the required magnetic performance under the actual site conditions. We review oil cooling when it is a better fit for the operating conditions.
An electromagnet uses electrical power to create its magnetic field, while a permanent suspended magnet does not need excitation power. Corvelan compares working distance, target tramp iron, running conditions, available power, cleaning needs and maintenance priorities before choosing the separator type.
Corvelan recommends a self-cleaning separator when tramp iron is frequent, captured metal must discharge automatically, or repeated cleaning stops would interrupt production. It also needs enough space for the discharge belt, drive, tracking, guarding and discharge path.
Start with the material, target tramp iron, throughput or conveyor loading, and a photo or drawing of the proposed installation point. Belt width, speed, material depth, particle size, environment, available power, cleaning preference and any test requirement help us select the separator and prepare the quotation.
You do not need a finished specification to start. Send the four items below. Corvelan will tell you which separator type fits the application and what other information we still need for an accurate quotation.
Corvelan will first confirm the separator type and the main installation and electrical connections. Then we will tell you what other data is needed for the final quotation.
Send the material, target tramp iron, conveyor loading and installation layout. Corvelan will check the separator type, working distance, cleaning method and main installation requirements before quotation.